Cangzhou Zhongtuo Roll Forming Machinery Co., Ltd.+86 13166567923steven@zt-rfm.com
Category

Tube Mill Auxiliary Equipment

5posts

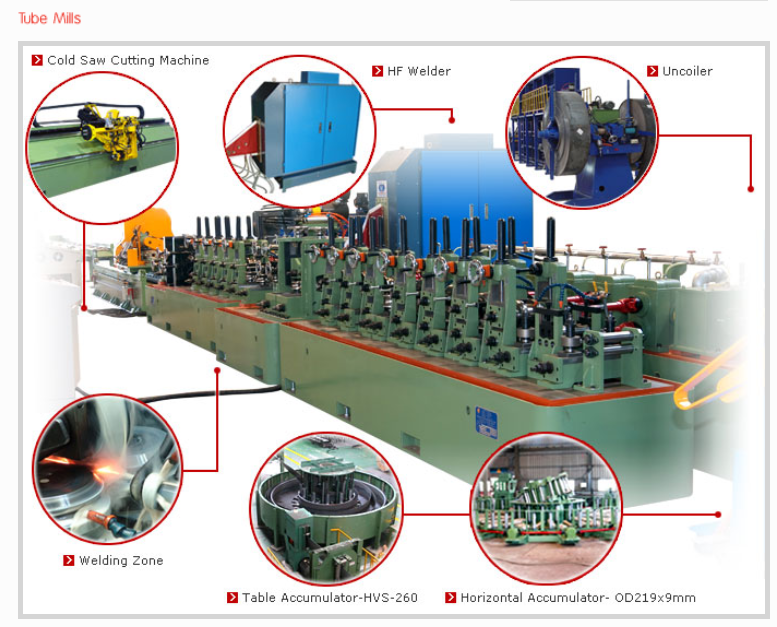
The units that complete a welded pipe line rather than make the pipe: uncoilers and decoilers, strip accumulators, shears and butt welders, run-out tables, cooling and straightening units, and the electrical control systems that tie them together. These are often bought separately when an existing line is extended or upgraded.

Datasheets for this group

What auxiliary equipment decides, and what it does not

Auxiliary equipment is everything on the line except the forming and welding section: coil handling in front, cut-off and run-out behind, and the tooling in between. It is usually chosen last, and it is usually what limits output first — a mill cannot cut faster than its saw returns.

Two items deserve to be specified at the same time as the mill rather than after it: the cut-off, which sets the cycle time, and the roll set, which decides which sections you can sell at all. Ordering these later is the usual cause of a line that runs well but cannot be sold into the sections the market asks for.

Matching the cut-off to the mill

A flying saw has to accelerate to tube speed, cut, and return before the next length arrives; that return time, not the forming speed, is what caps a short-length order. Ask for the cut-to-cut time at your shortest length, not only the maximum line speed.

The same logic applies to coil handling: a decoiler that needs a crane and fifteen minutes per coil change costs more per shift than a smaller mill running slightly slower. Coil weight and loading method are the numbers to settle first.

Chat on WhatsApp