Embossed Colour Steel Sheet Line — 0.5-1.0 mm, up to 1250 mm Width
This line presses a pattern into colour-coated steel sheet and recoils it.
82posts
Steel pipe machinery for a complete welded tube line: coil handling, roll forming, high-frequency welding, sizing, straightening, cut-off and run-out, plus the end forming and coil processing equipment around it. Machines are grouped here by process and by the tube diameter and wall they are built for — from 10 mm light-wall tube to 168 mm structural pipe.
This line presses a pattern into colour-coated steel sheet and recoils it.
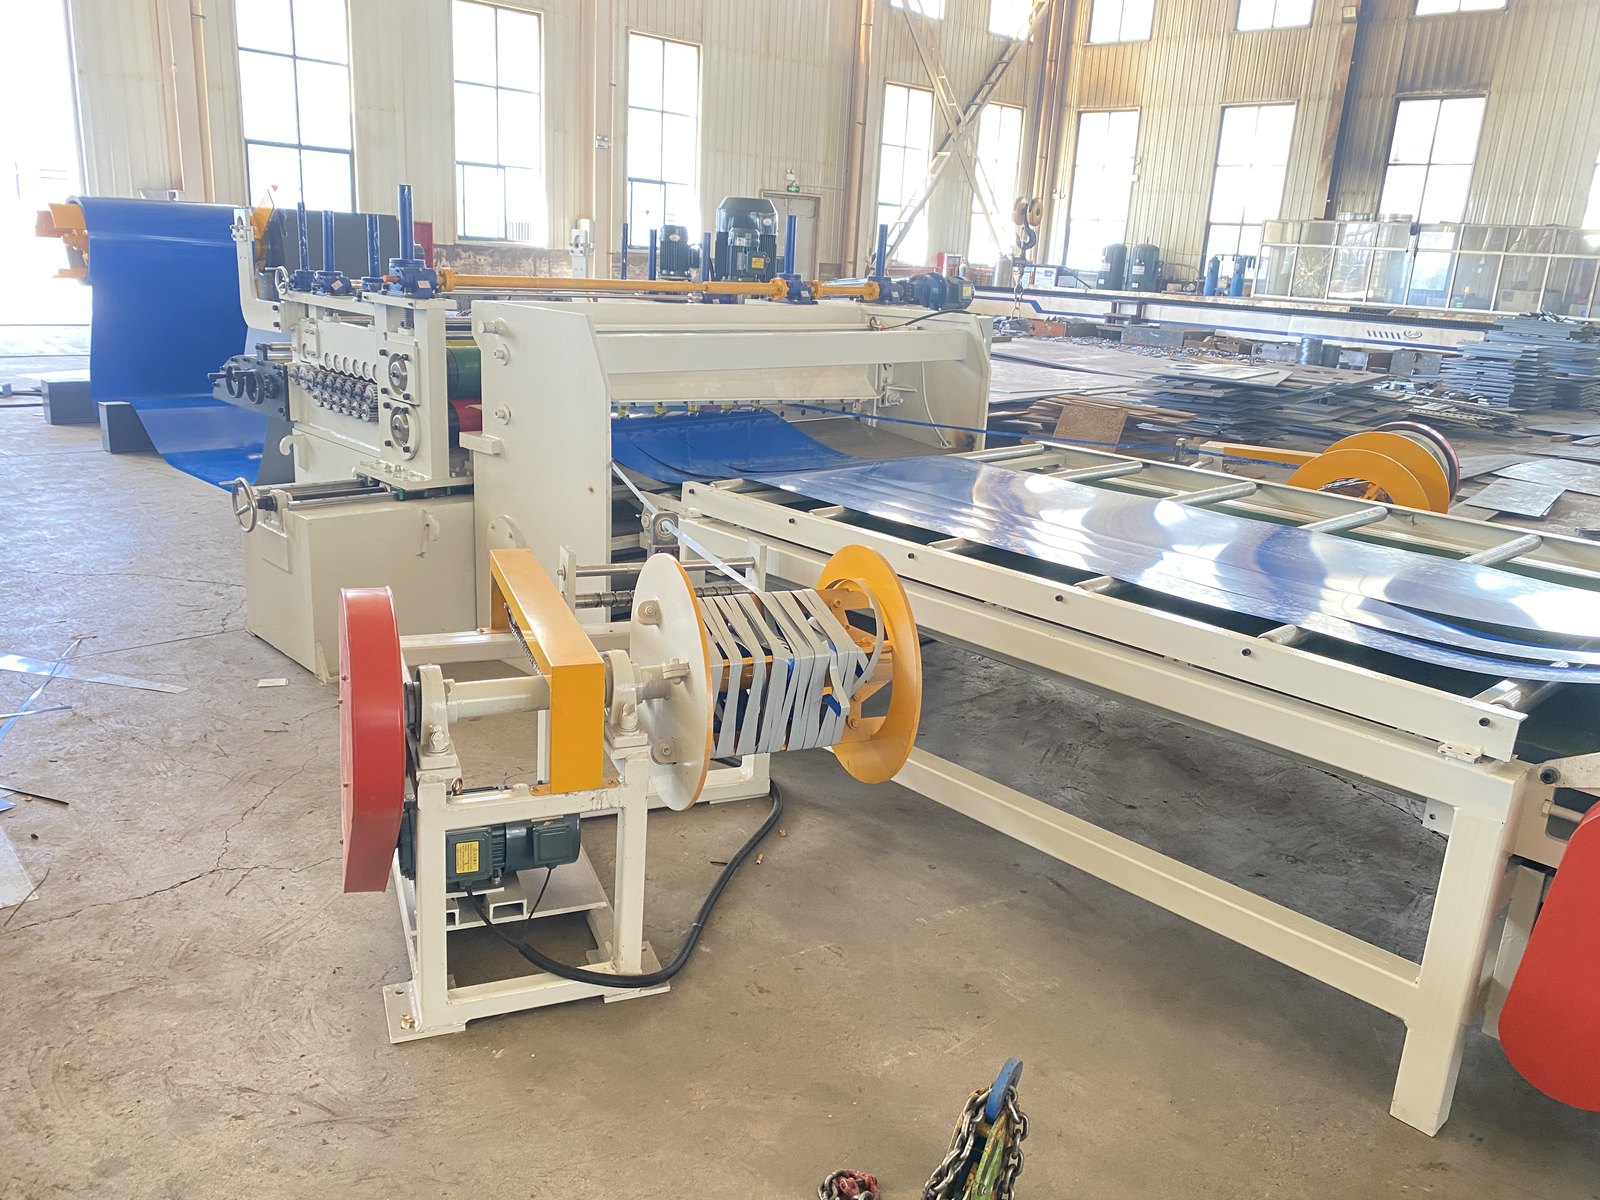
A slitting line cuts one wide steel coil into several narrow strips of a set width and recoils them under tension.
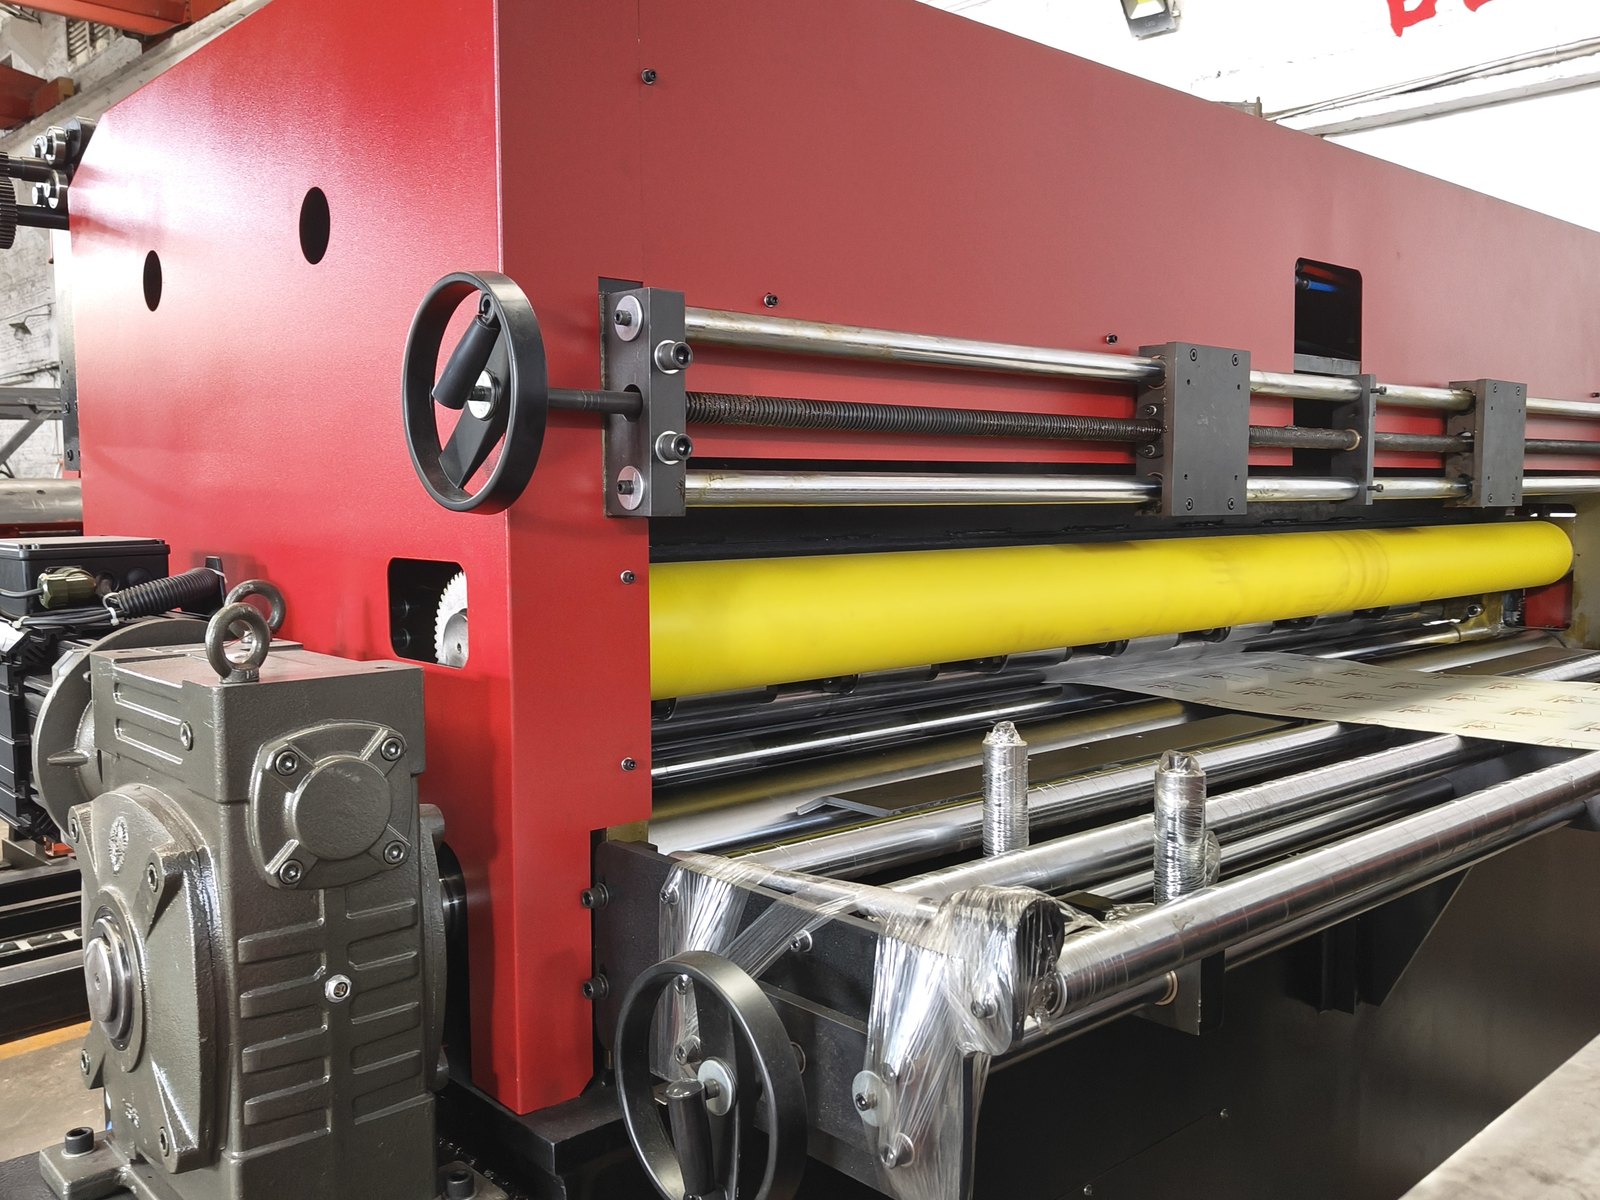
A cut-to-length line for aluminium coil up to 2600 mm wide and 1.5 mm thick: 15-roll four-high leveller, 4000 mm cut length and a 5 t decoiler with loading car.
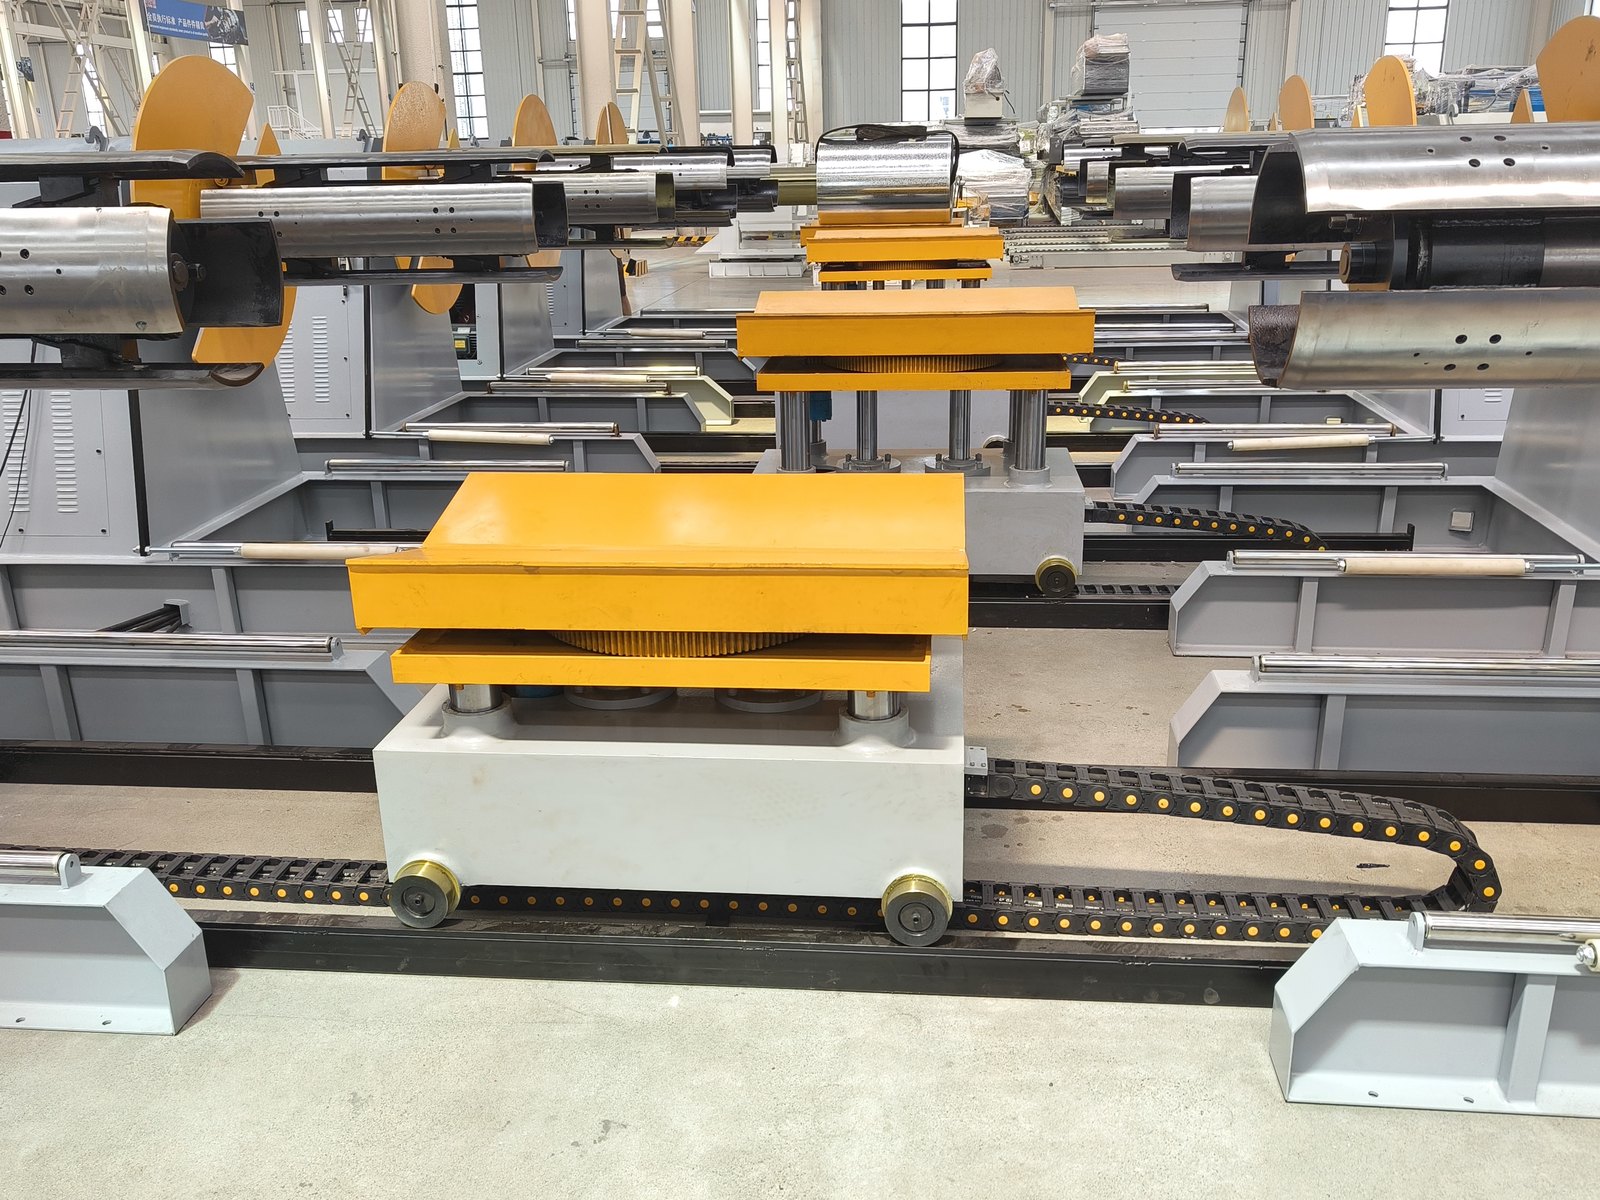
A 7 t hydraulic decoiler with its own loading car: expanding mandrel from 450 mm to 610 mm, coil up to 1250 mm wide and 0.4-1.0 mm thick, working speed 0-40 m/min.
A welded tube line built for one section: 30 x 30 mm square tube in 2.0 mm material, with the holes punched online in the line rather than on a second machine.
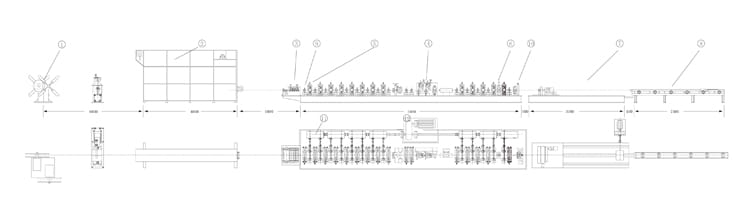
ZT series high frequency straight seam pipe making line: eight models covering 7-165 mm pipe and 0.3-5.0 mm wall at 15-100 m/min.
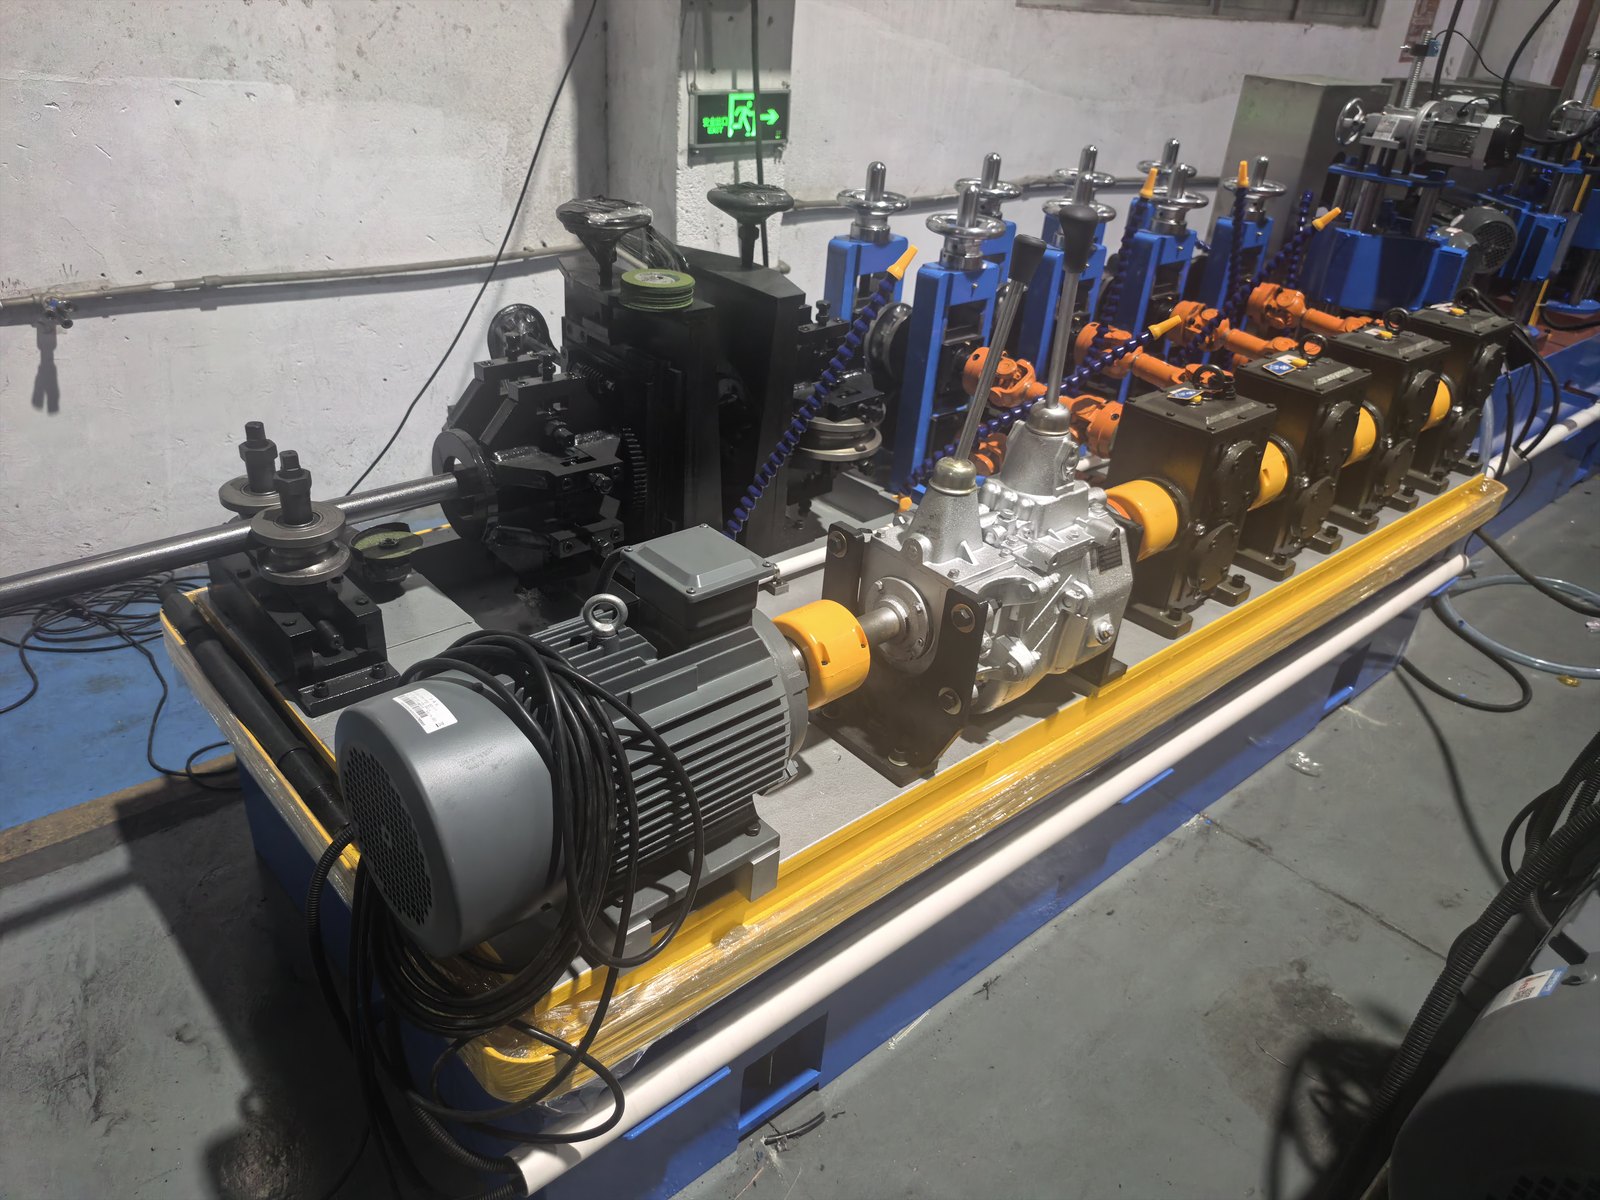
A 60-type tube mill that closes the seam with a 6000 W fibre laser instead of high-frequency induction.
A flying saw cuts tube to length while the tube keeps moving. ZF series cold cutting with servo tracing to +/-2 mm, plus the saw disc sizes published with the pipe lines on this site.
The feature of this HG76 Tube mill is high effective and durable. Specification range: 0.4mm wall, 40~50m/min.
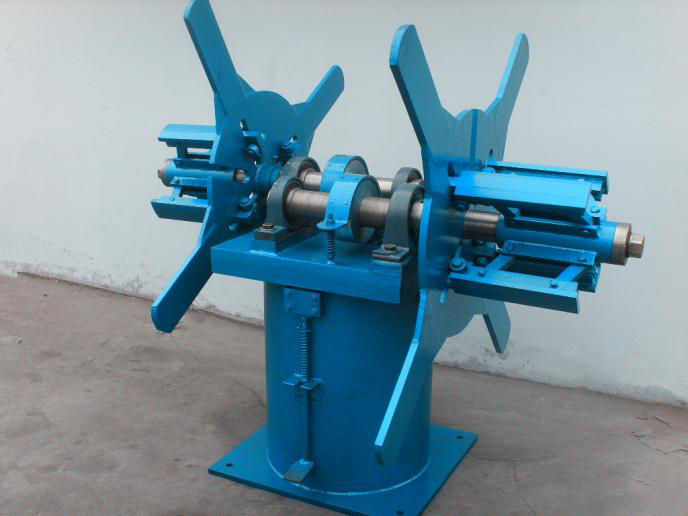
Operate: To put coil on the decoiler and then mandrel will expend by pneumatic system and fix the coil on the mandrel.
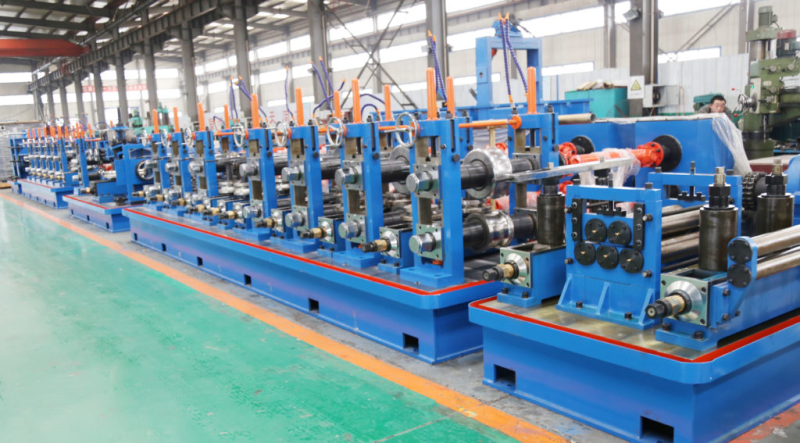
Steel pipe production line for 10-60mm welded pipe with 0.5-3.0mm wall: uncoiling, cage accumulator, forming, HF welding, sizing and flying saw.
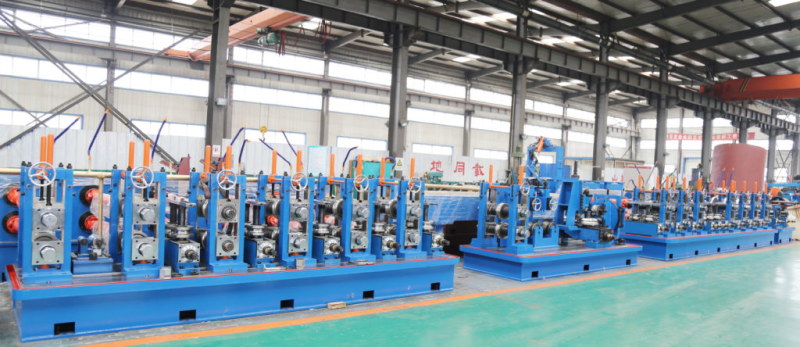
High frequency stainless steel pipe roll forming machine for round, square, rectangular and oval tube; the three stainless units on this site run at 3-7 m/min.
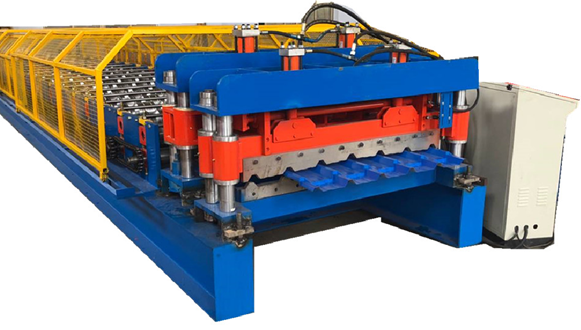
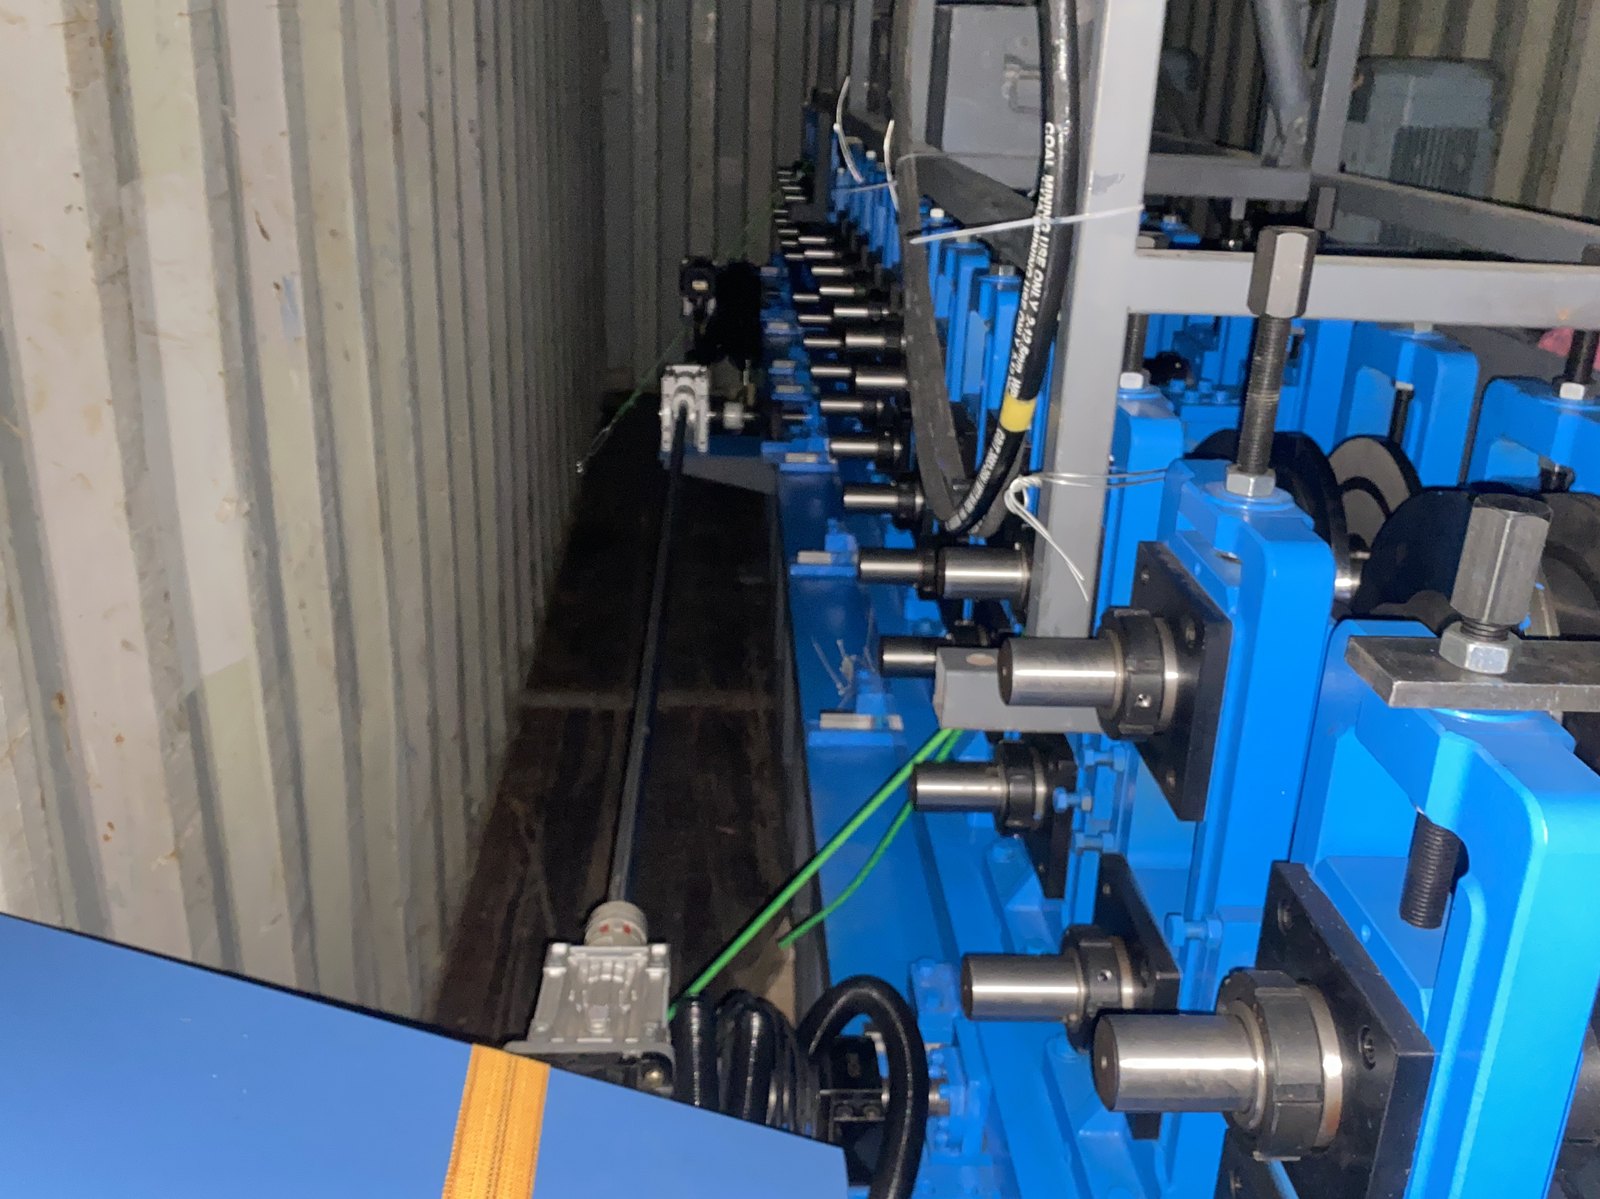
We will give the protection cover for Metal IBR tile making machine, when machine working.
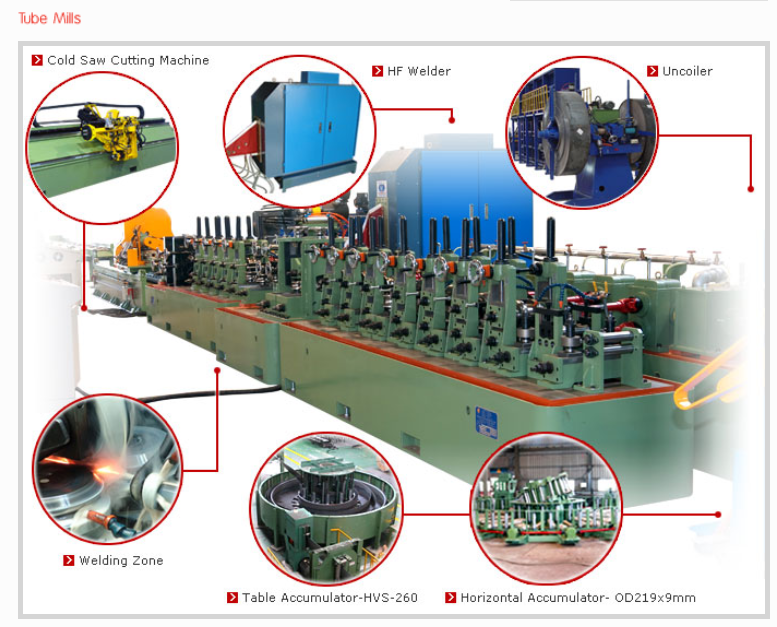
High frequency steel pipe making machine composes of a complete set of pipe forming machine, rotating capstan, decoiler, straightening machine.
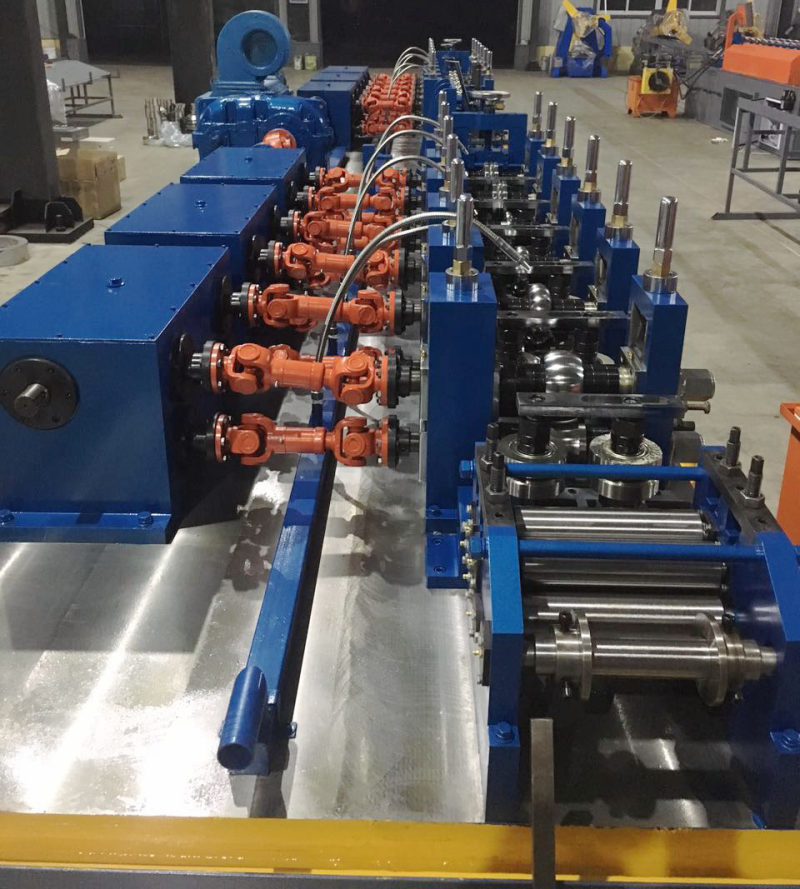
Now we have four types machines which are divided by wall thickness and diameter.
Features of the pipe line: two motors are automatically matched in speed, and gear box are adopted to enhance the torque force of transmission.
Stainless tube mills for 7-76 mm pipe ID and 0.3-1.5 mm wall: ZT-20C, ZT-30 and ZT-50, each published at 3-7 m/min, with the sealing and welding units that complete a stainless line.
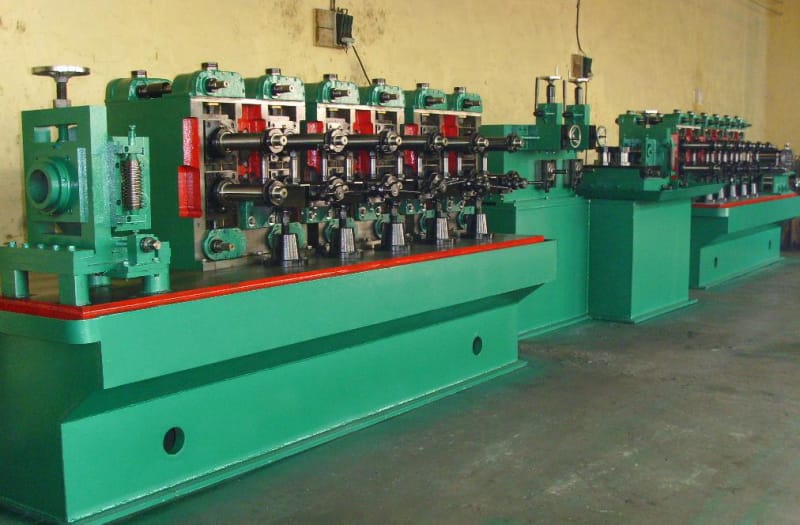
ZHONGTUO cold bending roll forming machinery factory is professional offering the high frequency welding pipe machines for making the round pipe.
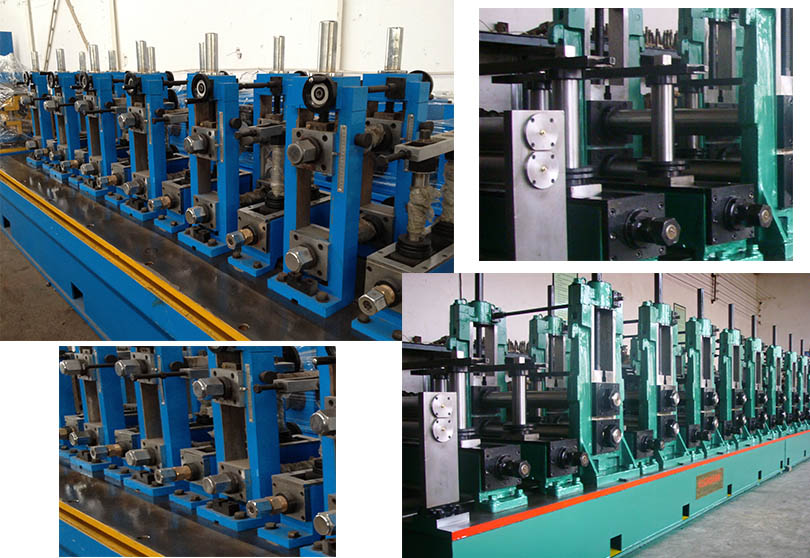
HG127 carbon pipe producer could be used to make pipes from diameter from 20-127mm within the wall thickness 1.0-4.0mm.
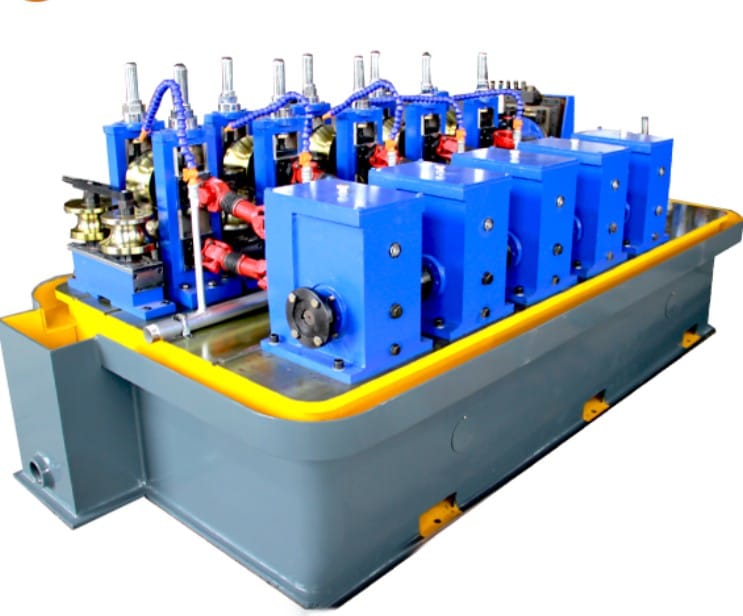
HG76 welded pipe making mill will be made to gantry type for processing large diameter pipe in a high speed.
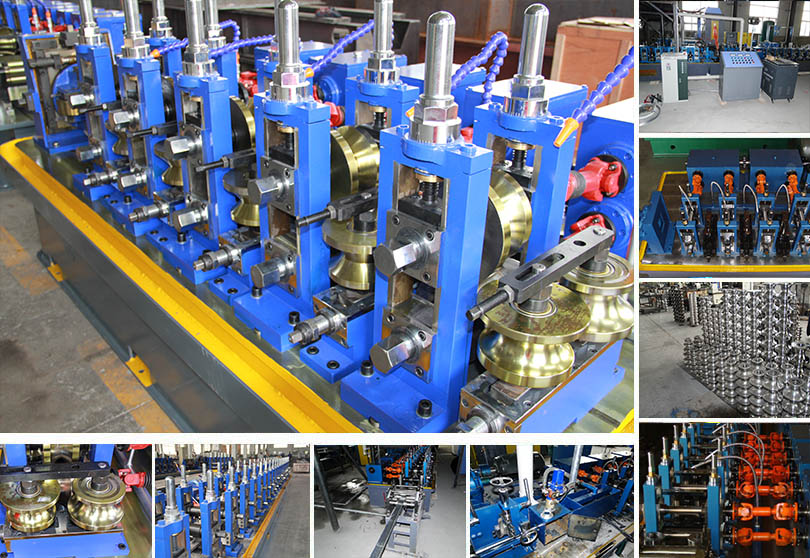
HG32 machine supports material thickness within 0.4-2.5mm, the diameter range from 10-45mm and the machine speed could make from 30-80m/min.
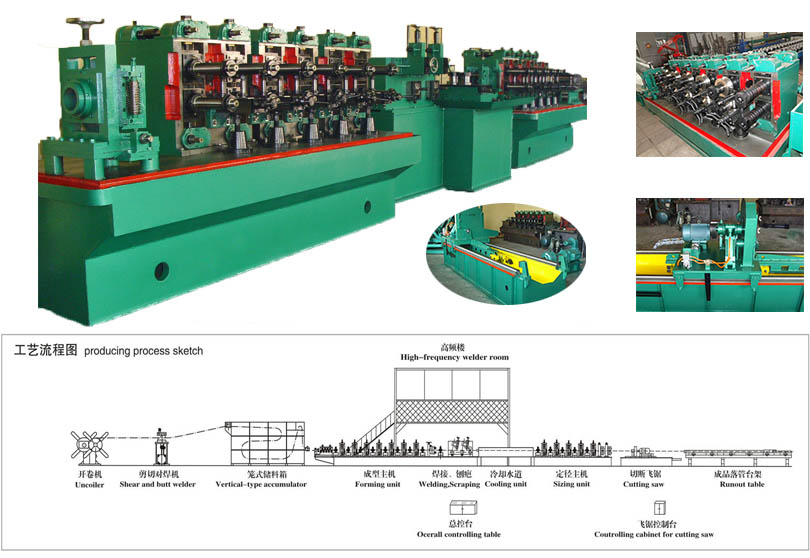
Here I will introduce HG50 welded pipe machine cantilever type. This machine is good for those who needs make various types small pipes within the wall.
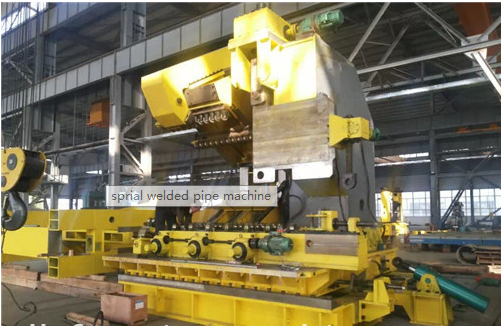
A spiral welded pipe machine makes large diameter pipe from coil: 160-3250 mm diameter, 2-10 mm wall, inner and outer welders, flying tracking cut-off car.
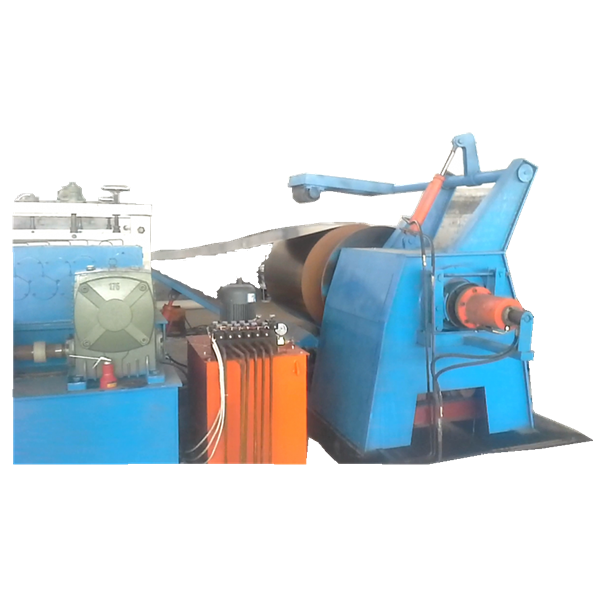
By cutting to length machine, we can make special length sheet from the coil no matter, color steel coil, glazined or iron.
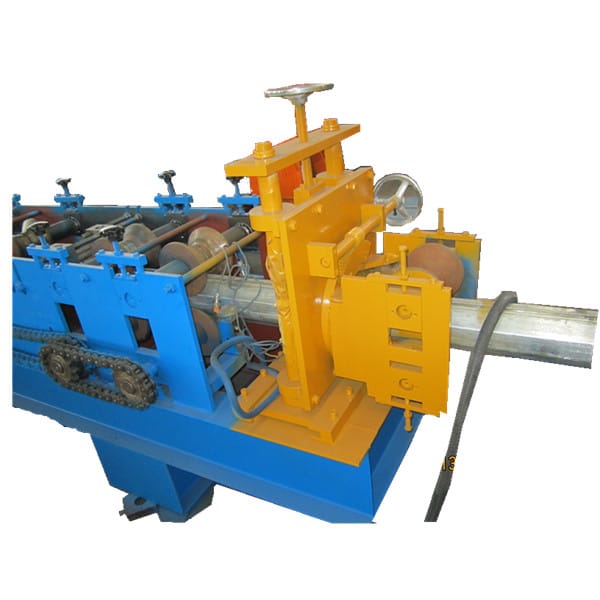
And the Octagonal Pipe is for roller shutters' tubular motor. Rolling shutter door & windows Octagonal tube.
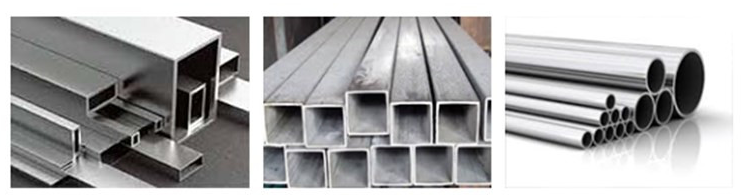
The tube rolling line is intended for manufacturing of round pipe of Φ16mm-Φ50mm with thickness of 0.5mm–2.5mm from cold-rolled and hot-rolled coil strip.
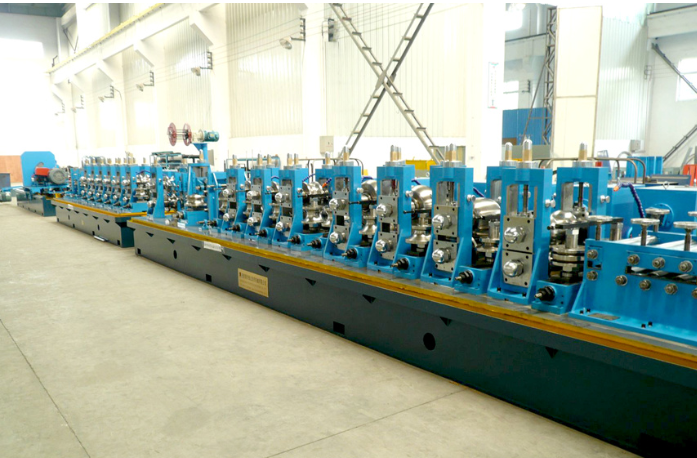
The mill is intended for manufacturing of round pipe of Φ76 mm-Φ168 mm with thickness of 2.0 mm–5.0 mm from cold-rolled and hot-rolled coil strip by means.
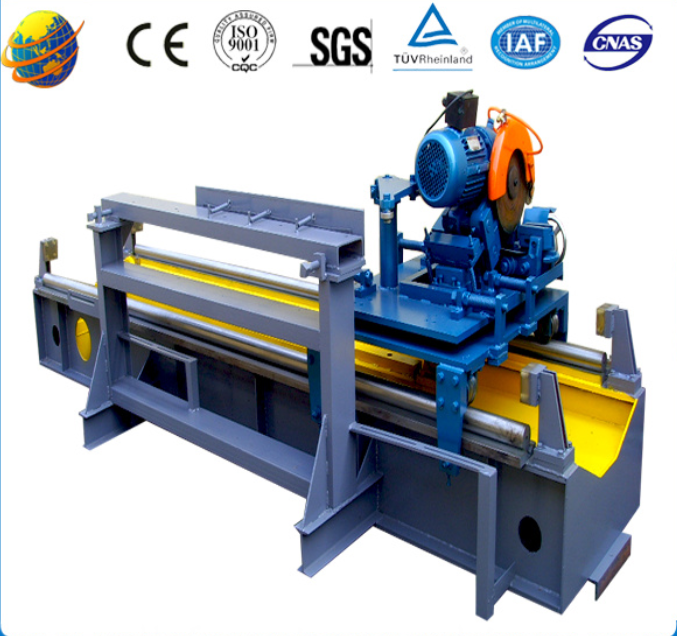
The mill is intended for manufacturing of round pipe of Φ38mm-Φ102mm with thickness of 1.0mm–5.0mm from cold-rolled and hot-rolled coil strip by means.
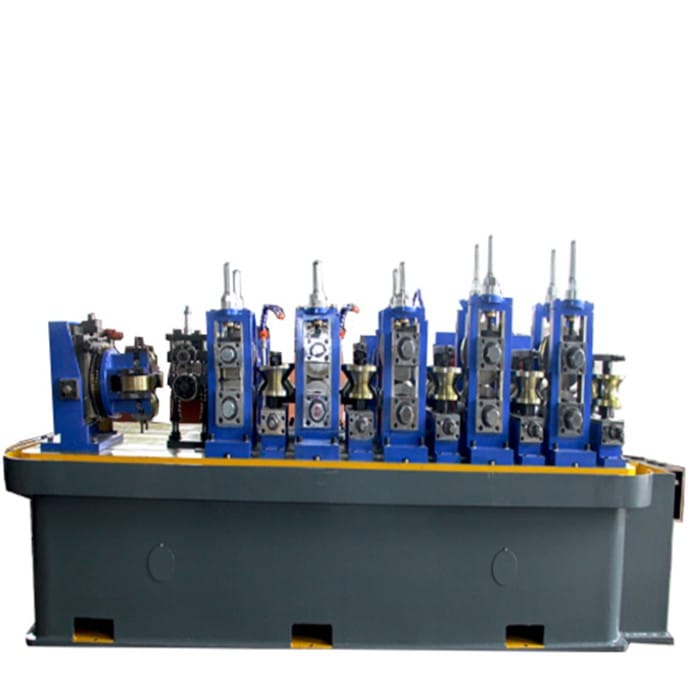
Zhongtuo HG32 welded pipe machine could make carbon steel pipe by roll forming principle. Specification range: 0.4-2.5 wall, 90m/min.
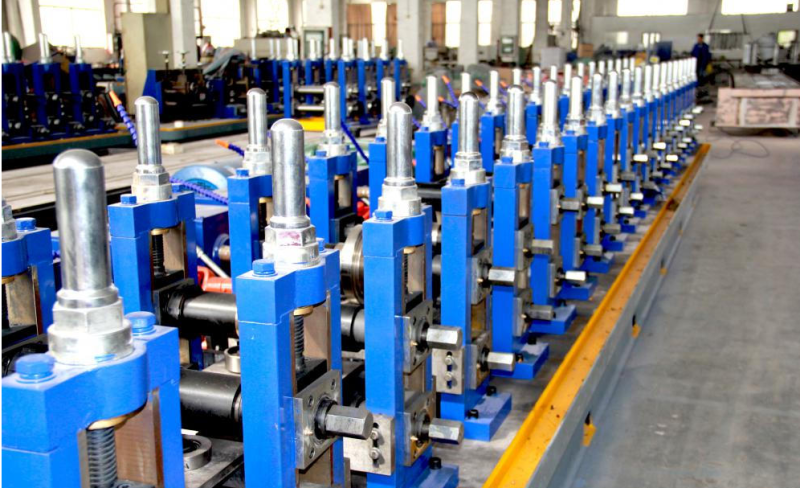
The mill is intended for manufacturing of round pipe of Φ20mm-Φ76mm with thickness of 1.0mm–3.5mm from cold-rolled and hot-rolled coil strip by means.
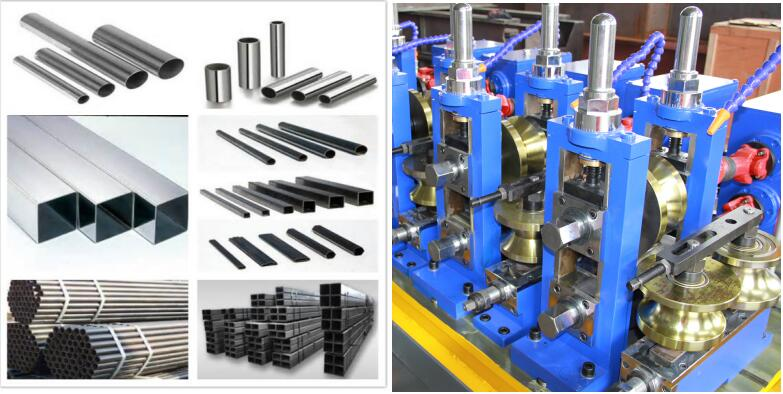
Zhongtuo steel pipe/carbon steel pipe processing equipment could be used to make steel pipe, carbon steel pipe by welding method.
Zhongtuo downspout pipe making machine could be used to make downspout pipes in a higher speed and good quality by 16 years in this area.
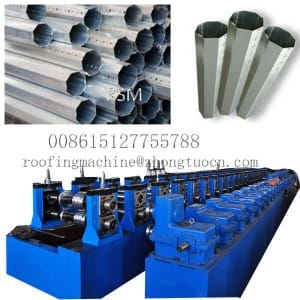
By the above Octagonal tube shape changing process, you can know how the tube is made from the strip.
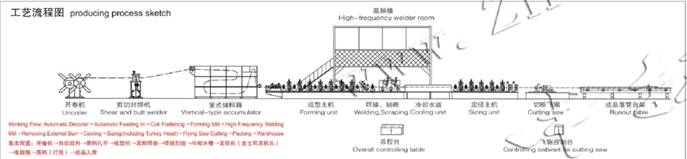
The mill is intended for manufacturing of round pipe of Φ10mm-Φ80 mm with thickness of 0.4mm–3.5mm from cold-rolled and hot-rolled coil strip by means.
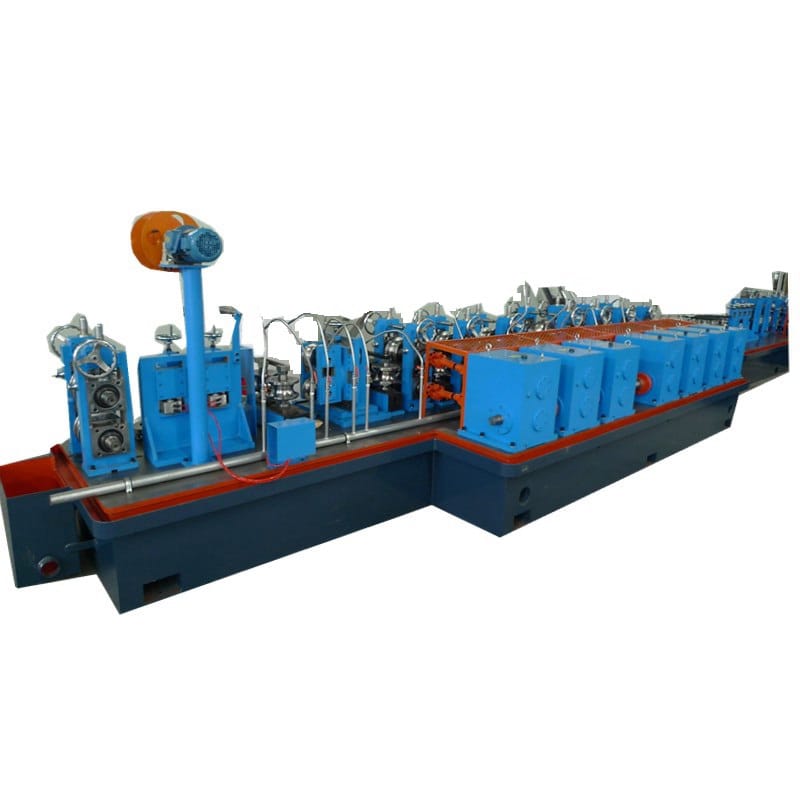
The machine is composed by the following elements: Double head uncoiler, hydraulic shearing and manual welding machine, Coiler feeder to accumulator.
Metal pipes made by rolling forming machine, normally has two type: welding pipes and interlocked pipe.
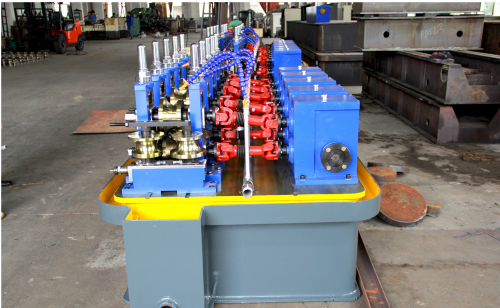
Annual output: 25000 ton, according to the yearly working days.daily working hours and the products. Specification range: 0.5–3.0mm wall, 30-90m/min.
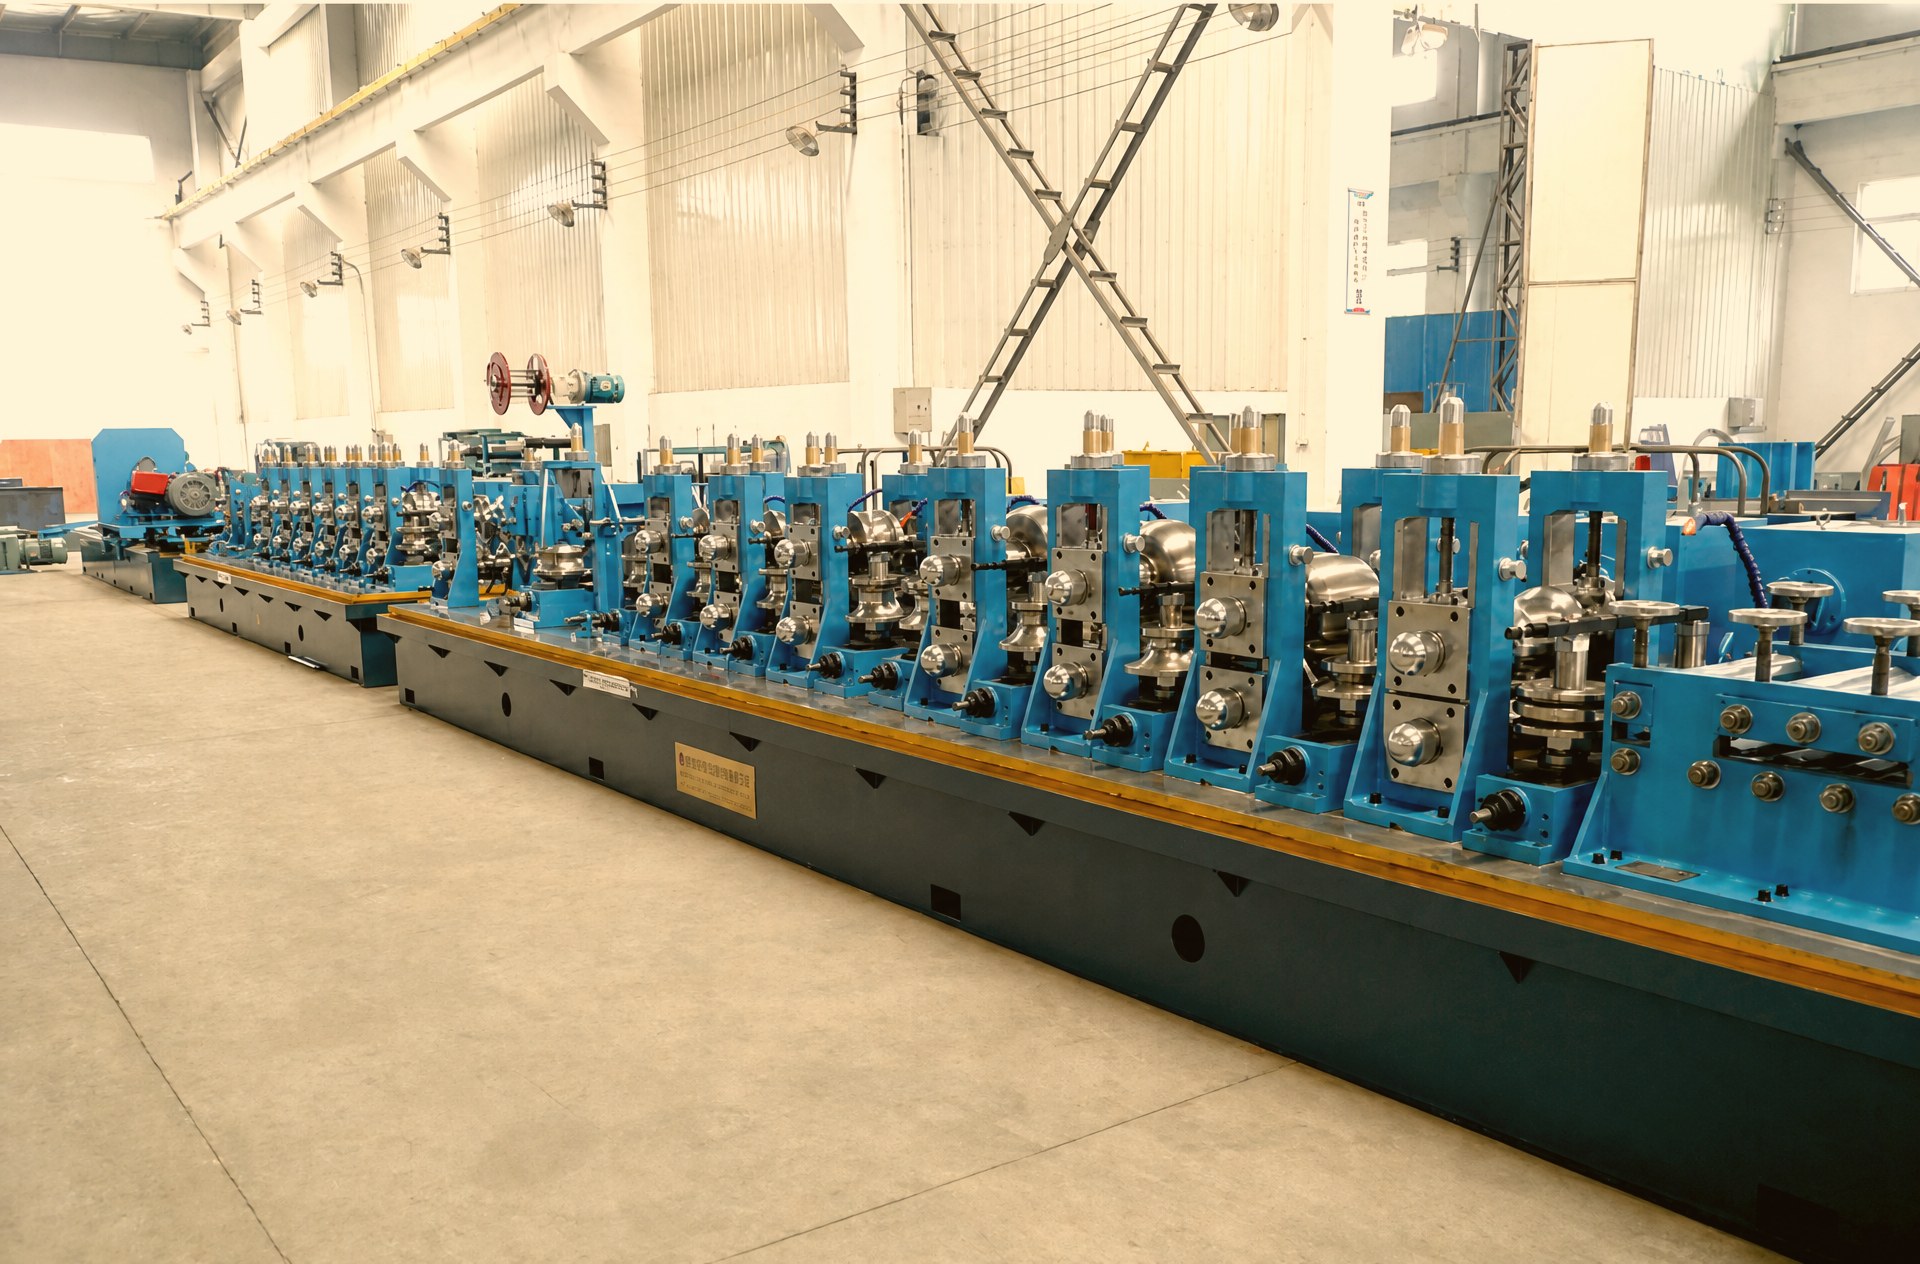
The mill is intended for manufacturing of round pipe of Φ20mm-Φ127mm with thickness of 1.5mm–5.0mm from cold-rolled and hot-rolled coil strip by means.
Welded steel pipe also called welded steel pipe, commonly they are made by steel or steel strip slitted by slitting line.
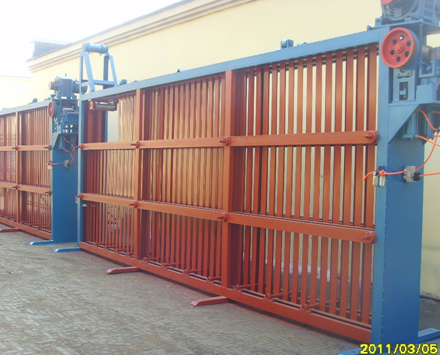
High frequency welding tube mill for square, round and oval pipe: one roll forming machine covers many sizes by changing moulds, with a 200 kW HF welder.
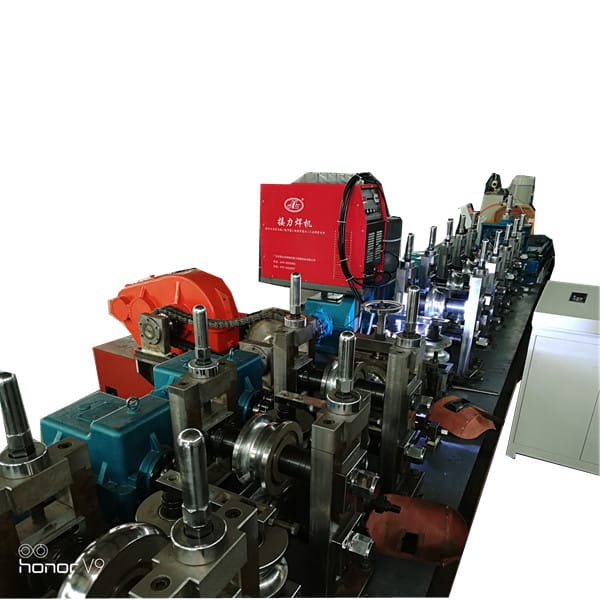
Argon arc welding is a welding technique that uses argon as a shielding gas. Also known as argon gas shielded welding.
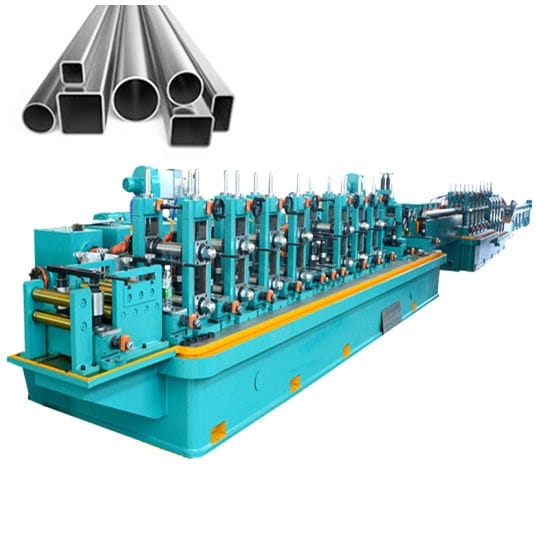
High Frequency Welding, known as Radio Frequency (RF) or Dielectric welding.
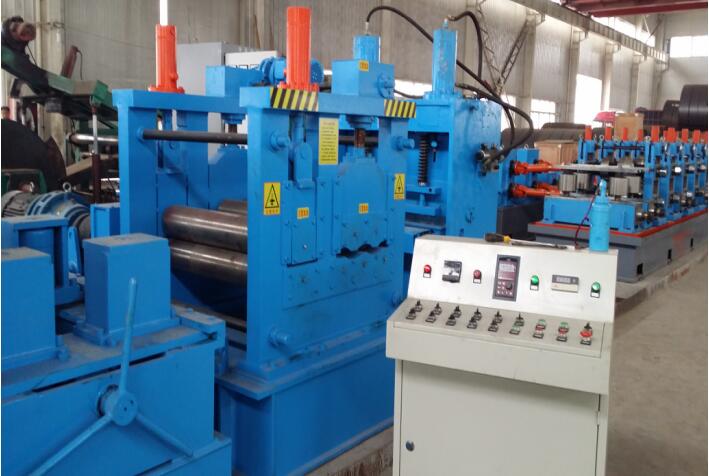
Tube making machine for multiple pipe sizes: round pipe diameter 38-127mm, 1.5-5.0mm wall, formed from cold-rolled and hot-rolled coil strip.
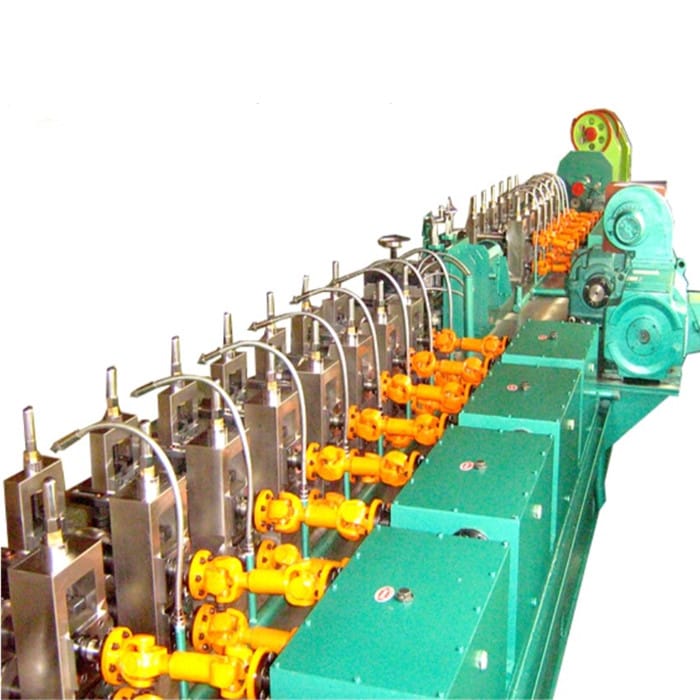
Automatic welded tube making machinery allows to do the production steel pipe, carbon steel pipe in batch fully automatically.
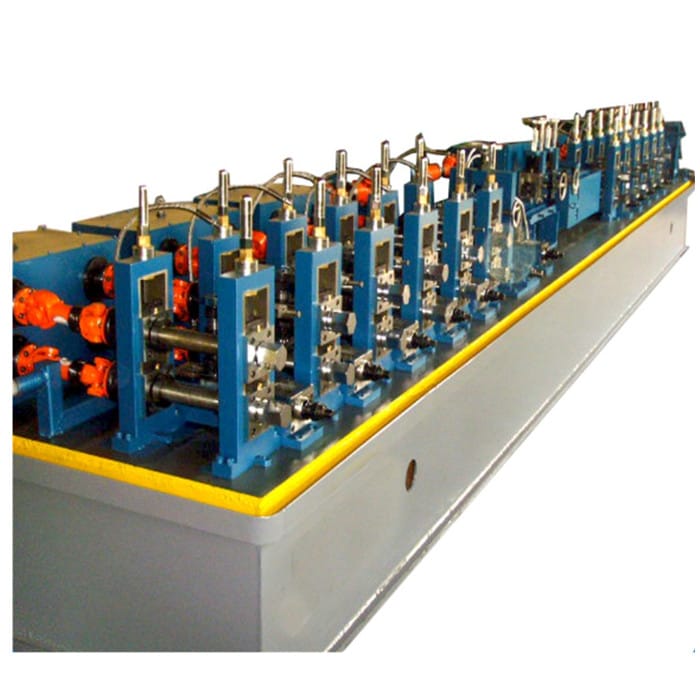
High frequency welded tube mill or welded pipe mill composes following elements like, single or double decoiler, leveling part machine, coil accumulator.
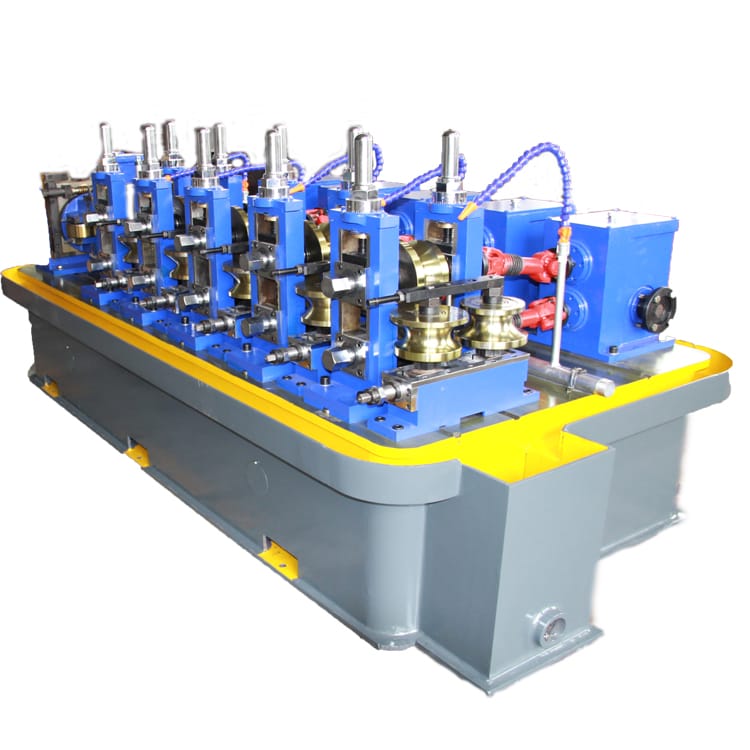
Fillet welded pipe roll forming machine: complete line with loading car, decoiler, unbender, two-roll coil feeder, cut-to-length machine and welding platform.
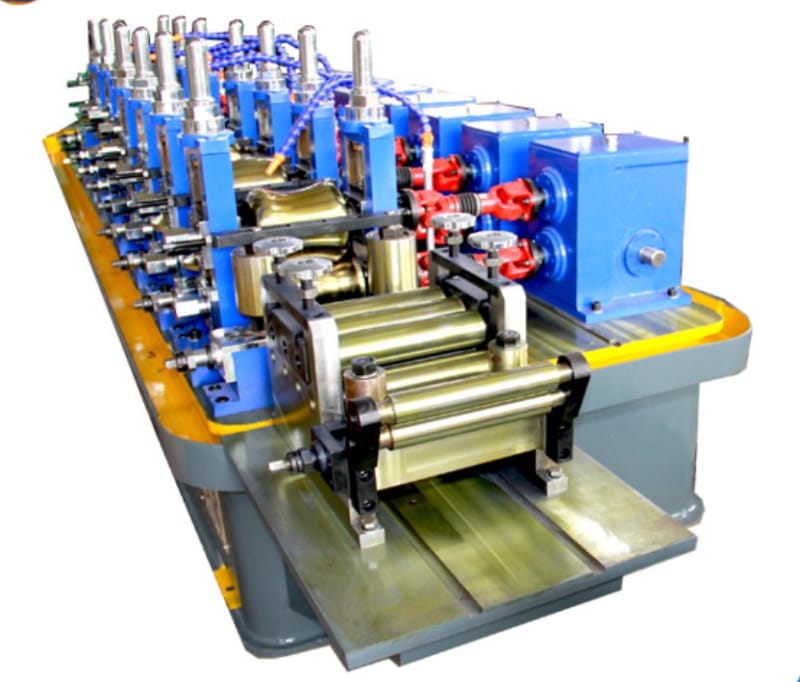
Our stainless welded pipe rolling former machine can produce many types of welded pipes, such as H32 H50 H76 H127.
The mill is intended for manufacturing of round pipe of Φ10mm-Φ89 mm with thickness of 0.4mm–6.0mm from cold-rolled and hot-rolled coil strip by means.
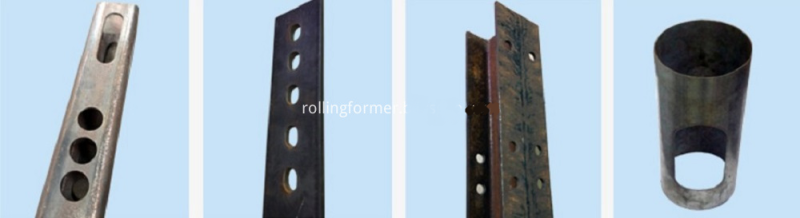
The Metal angle steel tube hole punching machine is a customized multicylinders punch machine.
V band clamp High precision exhaust band clamps bending machine is our new designed rollformer for the automobile exhaust tube clamping system.
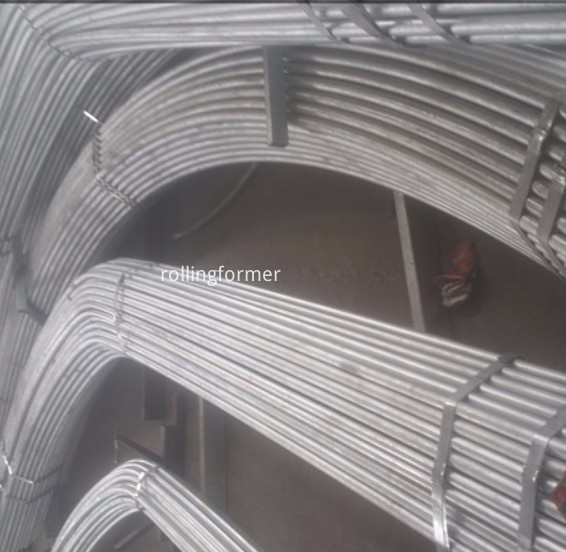
This product is mainly used for the construction of greenhouses, the construction of vegetable greenhouses.
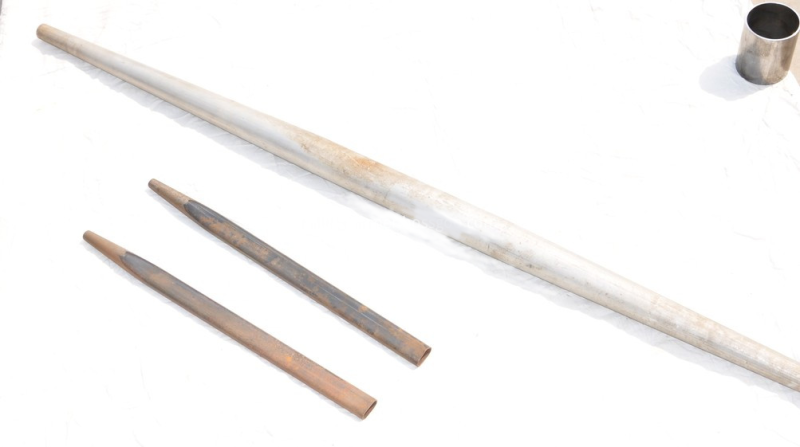
A pipe tapering machine forms a cone or taper on a steel tube end. ZSG50NCB is published for tube up to 50 x 2 mm, 300 mm forming length, 7-30 s cycle, 4 kW.
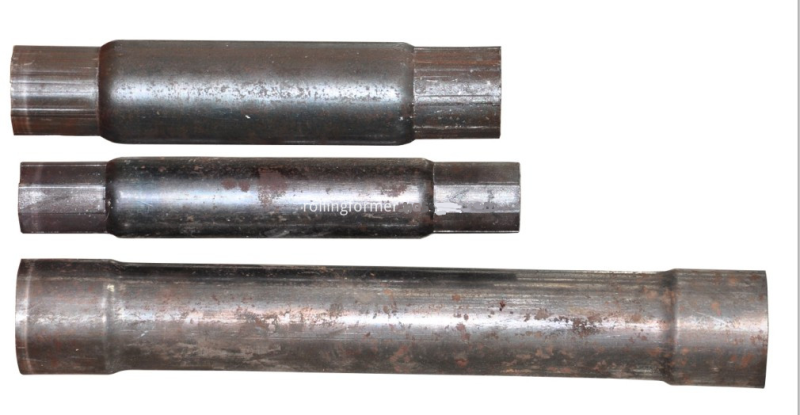
The C Type machines are designed for common end forming applications including tube expansion, tube tapering, reduction and slotting.
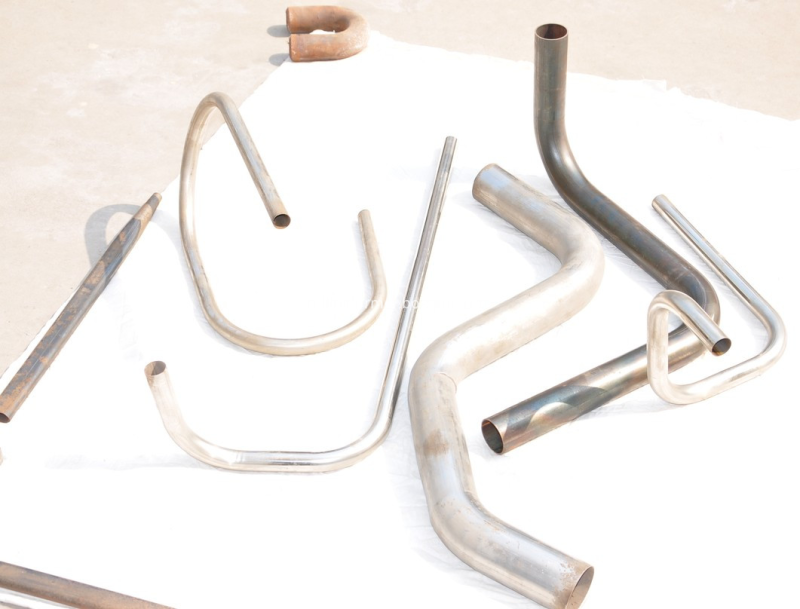
The CNC tube bender automatic tube bending machine is widely used, and there are different types of tube bending machines.
There are single head arc punching machine and double head arc notching machine of the single head arc punching machine Tube notching Machine.
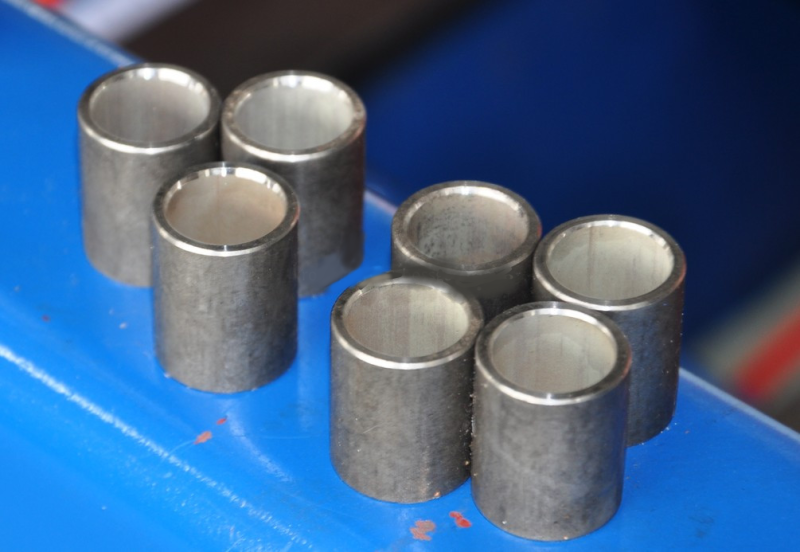
The portable chamfering machine hand chamfering machine is used to chamfer the iron tube with a correct and nice angle.
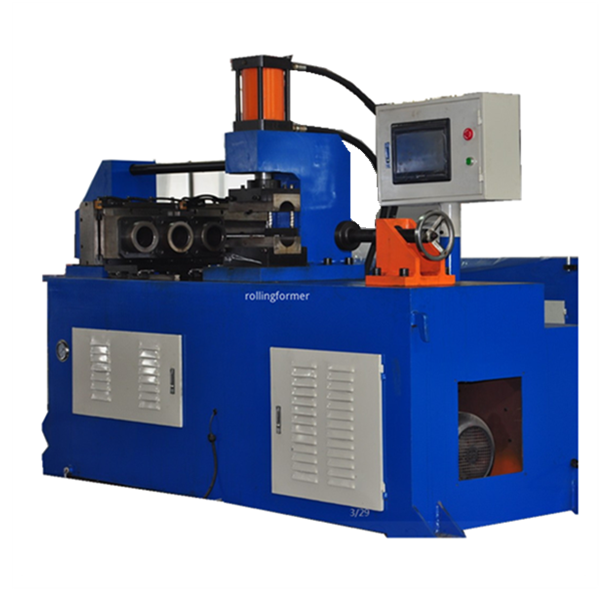
A tube reducer forms a smaller, larger or closed end on steel tube. Three stations, 16-165 mm with custom tooling, 110 mm forming length, 5-6 s cycle.
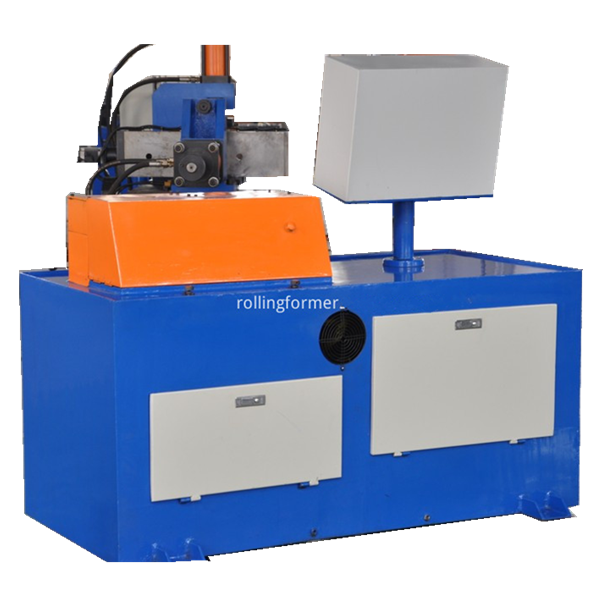
Tube closing machine for pipe end locking on 6-25.4mm tube with 0.5-2.0mm wall: hydraulic forming heads close tube ends without welding or sleeves.
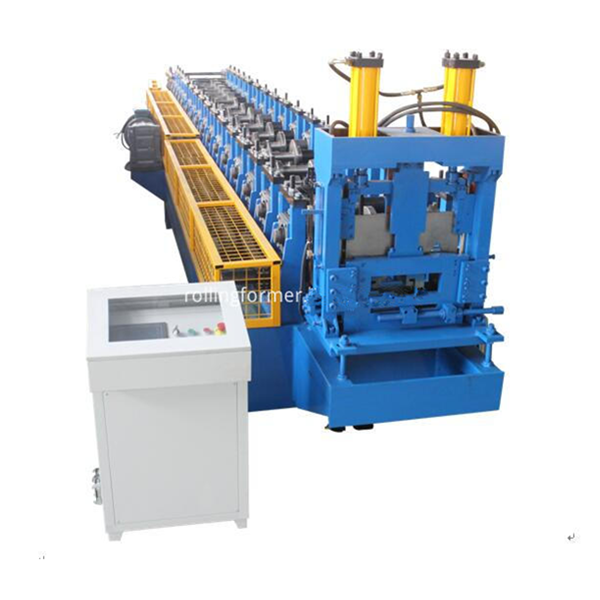
Yx15x40-80x100-300mm C purlin rollfomer machineis a line which can produce different sizes of C purlines by controlling the PLC.
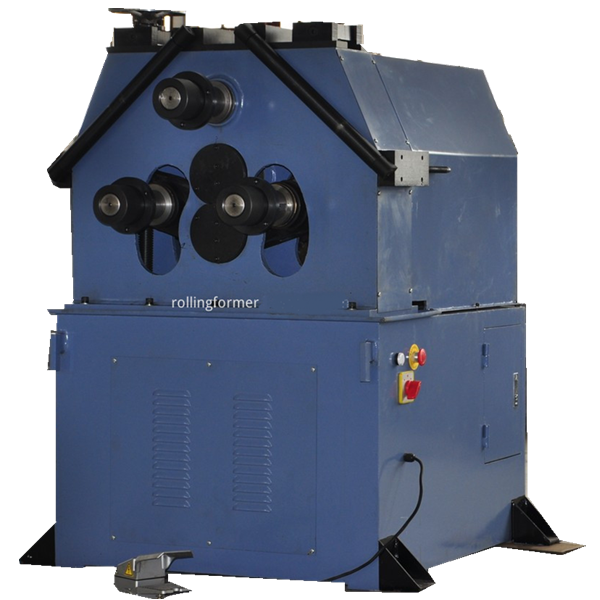
Full mechanical drive, compact construction, high reliability. Specification range: 3m/min.
ZT-25 high-frequency straight seam pipe-making line for pipe ID 8-32mm and wall 0.4-1.2mm at 30-100 m/min, with a 13-unit equipment list.
The ZT-50 covers pipe ID from 19mm-76mm, in wall thickness from 0.7mm-2.75mm, at line speeds of 30-100m/min.
ZT-28 high-frequency straight seam pipe-making line for pipe ID 10-50.8mm and wall 0.5-1.8mm at 30-100 m/min, with a 13-unit equipment list.
ZT-32 high-frequency straight seam pipe-making line for pipe ID 7-25mm and wall 0.3-1.0mm at 30-100 m/min, with a 13-unit equipment list.
The ZT-60 covers pipe ID from 25mm-80mm, in wall thickness from 1.0mm-3.25mm, at line speeds of 30m/min-100m/min.
The ZT-76 covers pipe ID from 30mm-90mm, in wall thickness from 1.0mm-4.0mm, at line speeds of 15m/min-70m/min.
The ZT-127 covers pipe ID from 32mm-127mm, in wall thickness from 1.5mm-4.0mm, at line speeds of 20m/min-70m/min.
The ZT-165 covers pipe ID from 50mm-165mm, in wall thickness from 2.0mm-5.0mm, at line speeds of 30m/min-50m/min.
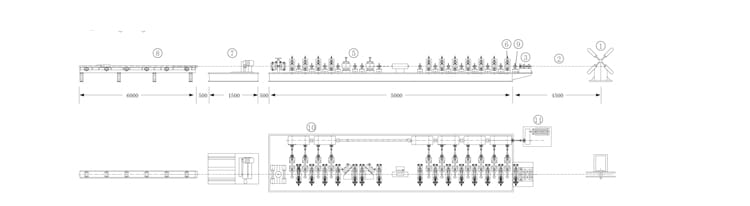
The ZT-20C covers pipe ID from 7mm-25mm, in wall thickness from 0.3mm-1.2mm, at line speeds of 3-7m/min.
The ZT-30 covers pipe ID from 13mm-30mm, in wall thickness from 0.4mm-1.5mm, at line speeds of 3m/min-7m/min.
The ZT-50 stainless covers pipe ID from 20mm-76mm, in wall thickness from 0.3mm-1.2mm, at line speeds of 3-7m/min.
The products produced are: 1.0 mm thick strip steel wrapped 7 mm metal calcium wire 9 mm seamless cored wire for the quality of modified steel in steel.
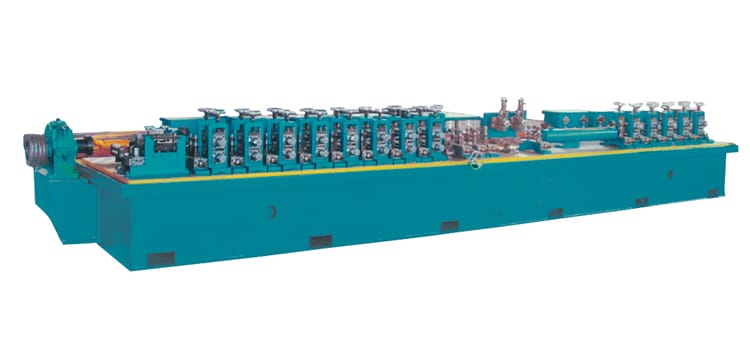
The GW series covers five sizes. Milling thickness ranges from 0.5~1.2 mm on the smallest model to 1.5~3.5 mm on the largest.
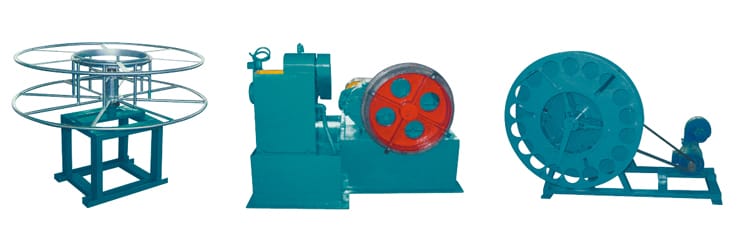
Wind the pipe in trolley with three-roller rolling device in the speed of pipe.
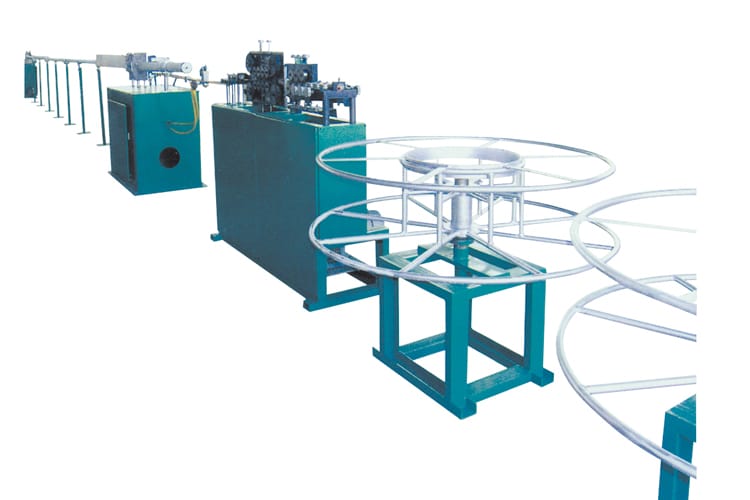
The drawing line reduces the diameter of welded pipe by pulling it through a die.
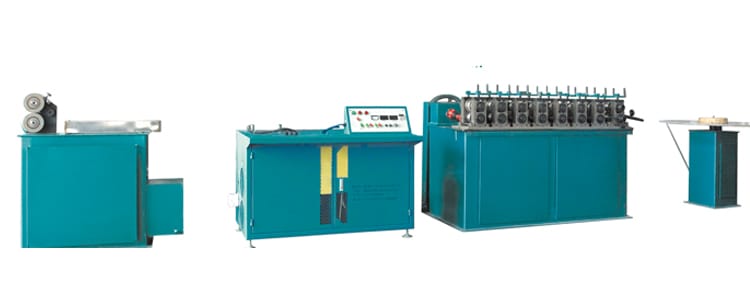
WZT Industrial frequency annealing production line. The line is delivered as 8 listed units.
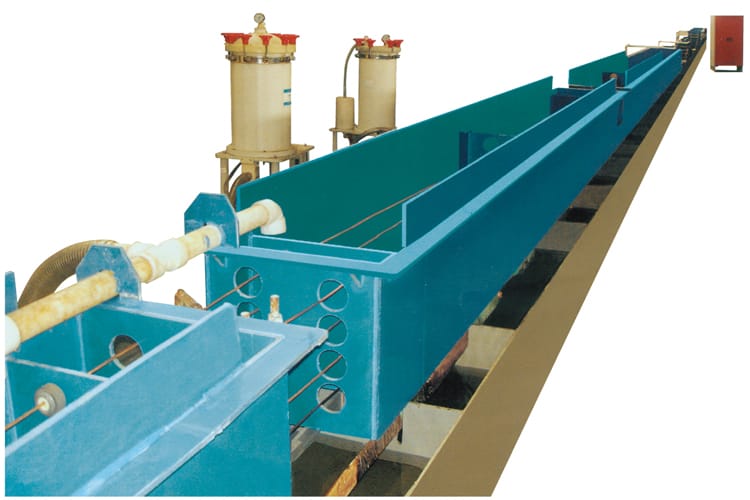
This line can contain 8 pipes(φ4~φ8) to coat zinc (copper) at the same time. Its design is advanced, reasonable, timesaving, cost saving, good usage effect.
Double layers brazing steel pipe (Bundy pipe) equipment introduction.
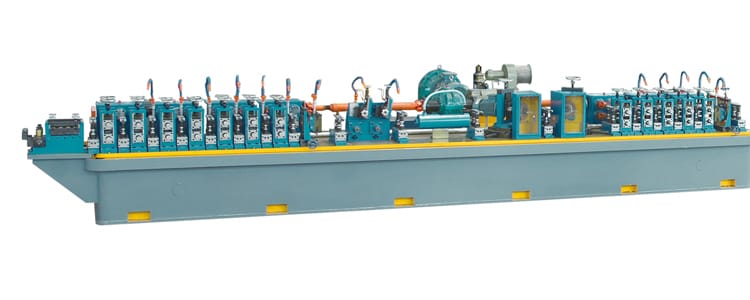
FG20/30 stainless steel cladding pipe mill line: FG20 runs 8-25.4mm tube with 0.3-0.5mm wall, FG30 runs 13-32mm with 0.4-0.8mm wall, both at 10-35 m/min.
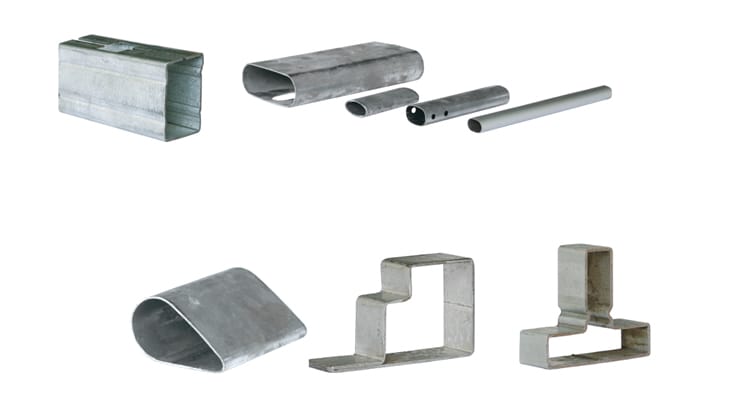
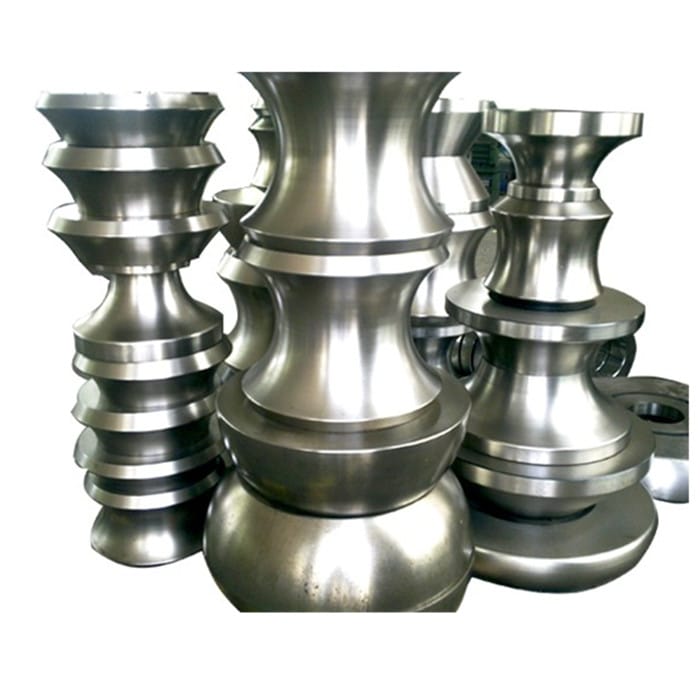
The rolls are the part of a welded pipe mill that actually shapes the tube.
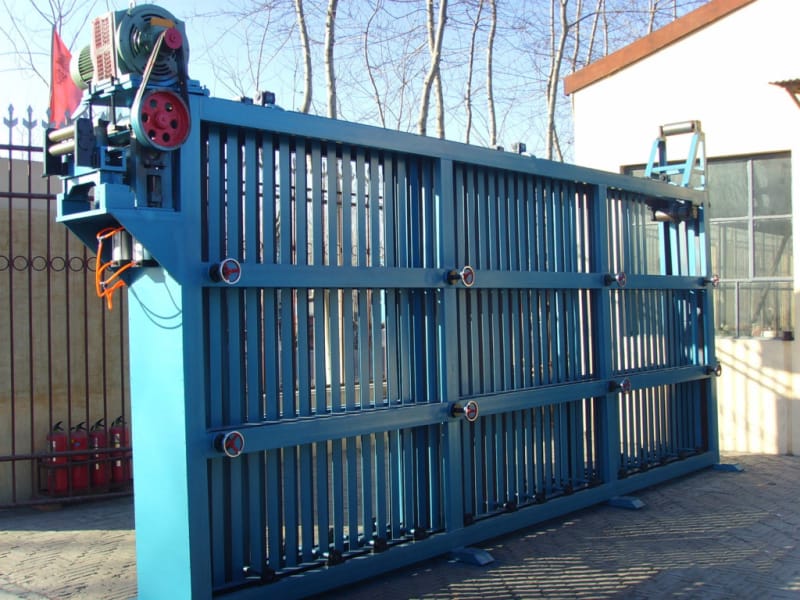
The storage unit holds a length of steel strip in a loop so the main machine can keep running while the ends of two coils are welded together.
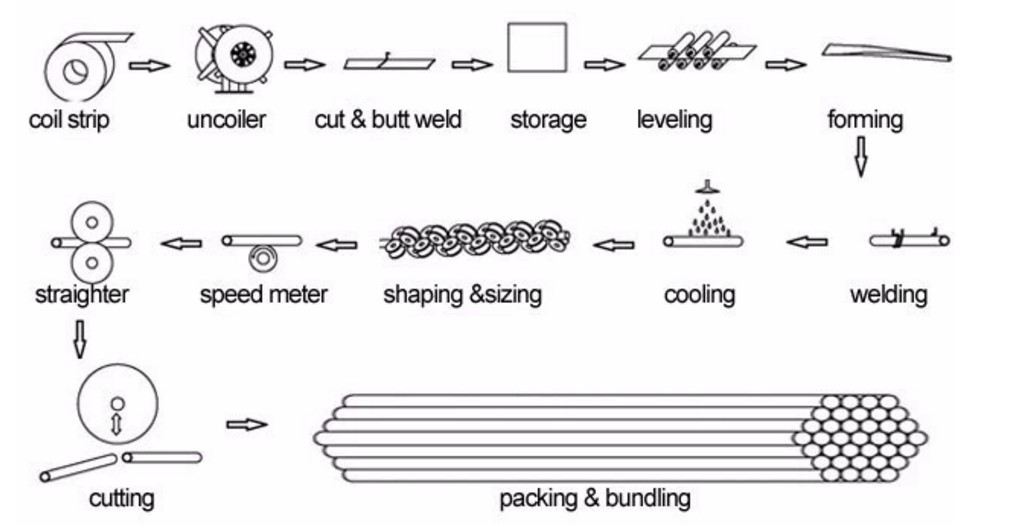
HG32 welded pipe machine: round pipe 10-45mm, square 7x7-35x35mm, rectangular 6x8-40x30mm, forming speed 30-90 m/min and a 30 kW main motor.
A tube line is five decisions, not one. Coil handling comes first: how heavy the coil is, how long a coil change takes, and whether strip is accumulated so the mill keeps running while a new coil is welded on. Then the forming and welding section, which sets the diameter and wall the line can make. Then sizing and straightening, which decide whether the tube is round enough to sell. Then the cut-off, which sets the cycle at short lengths. Then run-out and bundling.
Buyers often spend all their budget on the forming section and discover the binding constraint elsewhere — a saw that returns too slowly for short cut lengths, or a decoiler that needs a crane for every coil. Those two cost less than the mill and are much cheaper to specify up front than to change later.
The forming section is built for a diameter band and a wall range; asking it to run outside that band is a roll-load question, not a setting. So the specification should start with the finished tube: outside diameter, wall, round or square or rectangular, cut length, and how many tonnes a month. Everything else follows from those numbers.
Where a product range straddles two machines, the usual answer is the wider machine run slower on small sizes — unless the small sizes are high volume, in which case two lines are cheaper in the long run. A drawing or a section list is the fastest way to an accurate quotation; a model number alone is not.