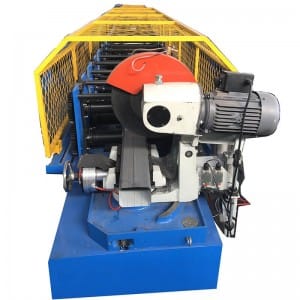
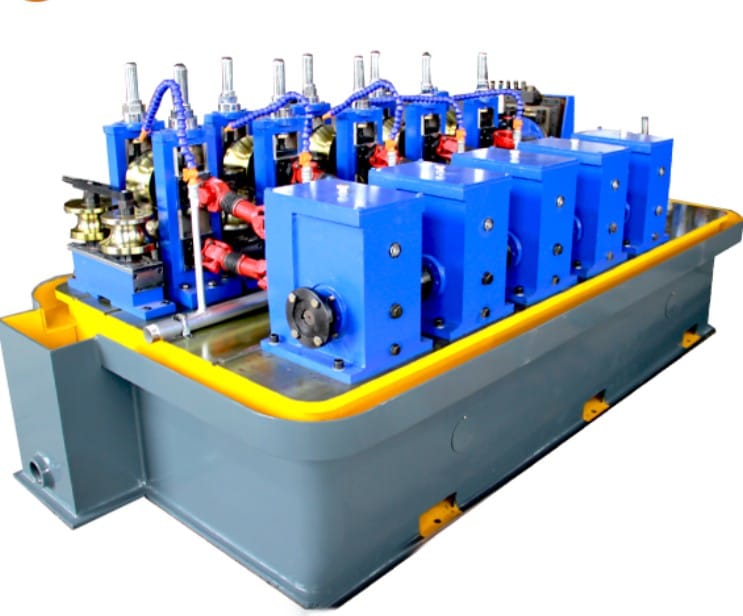
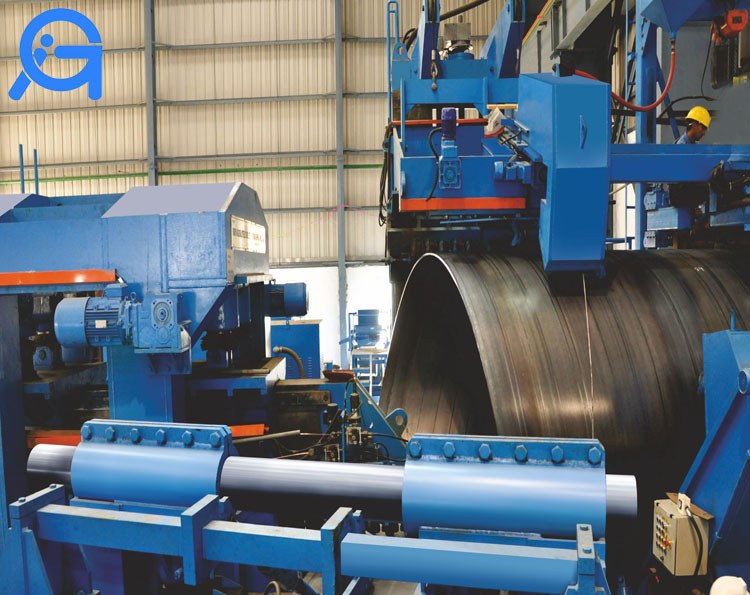
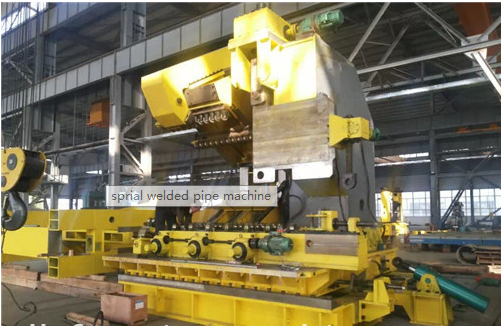
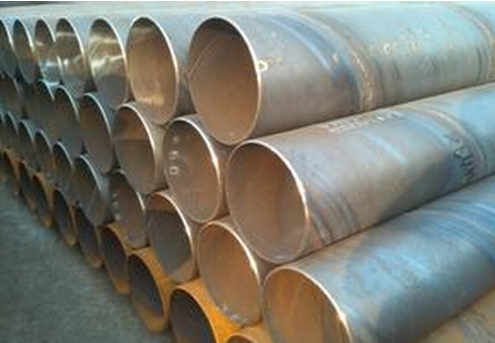
A spiral welded pipe machine makes large diameter pipe from steel coil. The strip is uncoiled and levelled, the coil end is joined to the previous one, then the strip is fed into the forming section at an angle so the edges meet in a helix. Inner and outer welders close the seam as the pipe advances, and a flying tracking car cuts the finished pipe to length without stopping the line.
Because the pipe diameter comes from the strip width and the forming angle rather than from a fixed set of forming rolls, one machine covers a very wide diameter range — the range published for this machine is 160 mm to 3250 mm.
Specifications
Parameter | Value |
|---|---|
Pipe diameter range | 160-3250 mm |
Wall thickness range | 2-10 mm |
Materials | Galvanized sheet, carbon steel coil |
Coil handling | Decoiler with leveling rollers stressed by hydraulic cylinders |
Coil end joining | Cutting edge and welder system with loading car |
Edge trimming | Disc shearing with waste edge scrap boxes (1 shear, 2 scrap boxes) |
Forming | Roll forming machine with stabilizer and rear/front axle devices |
Welding | Inner and outside welders |
Cut-off | Flying tracking cutting car (non-plasma cutting) |
Foundation | Buried parts foundation supplied with the machine |
Diameter and thickness above are the published ranges. Strip width, forming angle, line speed and welding procedure for a given pipe size are worked out from your specification and confirmed at quotation.
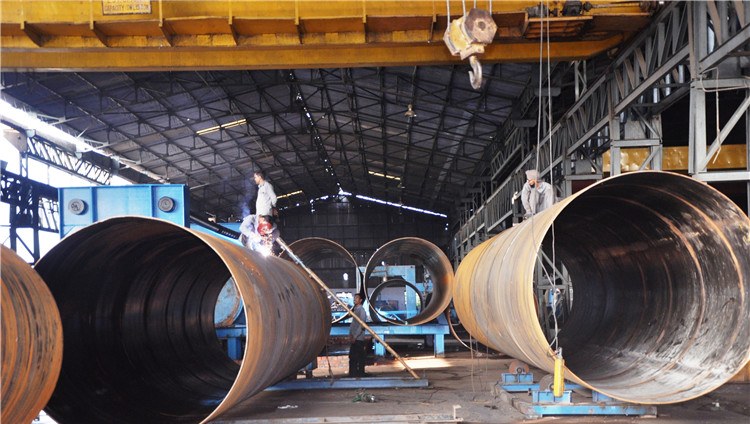
Working process
Decoiling, then removing the unneat and unstraight part at the start of the coil; feeding the coil into the machine; vertical rollers hold the strip and the coil end is welded to the previous coil; the strip passes through leveling and edge shearing; pre-bending sets the curvature; the strip enters the forming section at the spiral angle; the seam is welded inside and outside; and the finished pipe is cut by the flying tracking car.
Where spiral pipe is used
Transmission piping for high-intensity petroleum and natural gas to API standard.
Low-pressure fluid transfer, city gas and drainage pipelines.
Pile driving tube for construction projects.
Steel tube for industrial structures.
Main elements of the machine
No. | Element |
|---|---|
1 | Double head style |
2 | Shovel head device |
3 | Coil feeder system with vertical roller system |
4 | Cutting edge and welder system with loading car (removes edge, welds two edges) |
5 | Horizontal guide device, electric vertical roller |
6 | Disc shearing and waste edge scrap box (1 shearing, 2 scrap boxes) |
7 | Coil delivery system |
8 | Pre-bending system to make the coil curve |
9 | Entrance guide |
10 | Entrance roller |
11 | Roll forming machine |
12 | Rear axle device |
13 | Stabilizer |
14 | Flying tracking cutting car (non plasma cutting) |
15 | Swing and supporting rollers |
16 | Front axle device |
17 | Inner and outside welders |
18 | Foundation for buried parts |
19 | Hydraulic system |
20 | Electrical system |
Documents and site work supplied with the machine
After the contract is signed the seller supplies the foundation drawing for the buried parts and the building detail drawing, a foundation plan (including the arrangement of water, electricity and air), an arrangement plan, and the operation instruction covering structure diagrams, operation, maintenance, troubleshooting, safety rules and consumables.
Installation and commissioning are supervised on site by the seller's engineers, who start within 10 days; commissioning takes about 3 engineers over 30 days, the buyer's operators are trained during commissioning, and acceptance is signed off in the certificate of acceptance. International air tickets and local costs (board, lodging, daily transport, communication, insurance) are on the buyer, and the buyer provides an interpreter.
Frequently asked questions
What diameter pipe can a spiral welded pipe machine make?
The machine on this page is published for 160 mm to 3250 mm diameter with 2 mm to 10 mm wall thickness. Because the diameter comes from strip width and forming angle, one machine covers that whole range.
What materials does it run?
Galvanized sheet and carbon steel coil, as published on the machine page.
How is the pipe cut to length?
By a flying tracking cutting car, which is a non-plasma cutting machine — the car travels with the pipe so the line does not stop for each cut.
Related pages: coil processing lines, HF pipe welding machines, steel coil slitting line