A slitting line cuts one wide steel coil into several narrow strips of a set width and recoils them under tension. The line takes cold-rolled, galvanized and hot-rolled coil, and it sits upstream of tube mills, roll forming lines, panel lines and blanking operations whenever the incoming coil width does not match the finished part.
Two standard configurations
Parameter | SL-1250 | SL-1600 |
|---|---|---|
Strip material | Cold-rolled, galvanized sheet | Galvanized, cold-rolled, hot-rolled coil |
Strip thickness | 0.3-3.2 mm | 0.35-4.0 mm |
Coil width | 600-1250 mm | up to 1600 mm |
Coil inner diameter | 508 mm | 508 / 610 / 750 mm |
Coil outer diameter | max 1600 mm | max 1600 mm |
Coil weight | max 12 t | max 15 t |
Coil camber | — | max 2 mm/m |
Slit strip width | from 20 mm | — |
Width tolerance | +/-0.05 mm | +/-0.05 mm |
Line speed | up to 25 m/min | threading 10 m/min; 10-20 m/min |
Line footprint | — | 20 m x 8 m (L x W) |
Supply | AC 380 V +/-10%, 50 Hz +/-5%, 3-phase 5-wire | — |
Air supply | 0.4-0.6 MPa | — |
Other thickness and width ranges are built to order — send us your coil schedule and we will confirm the configuration.
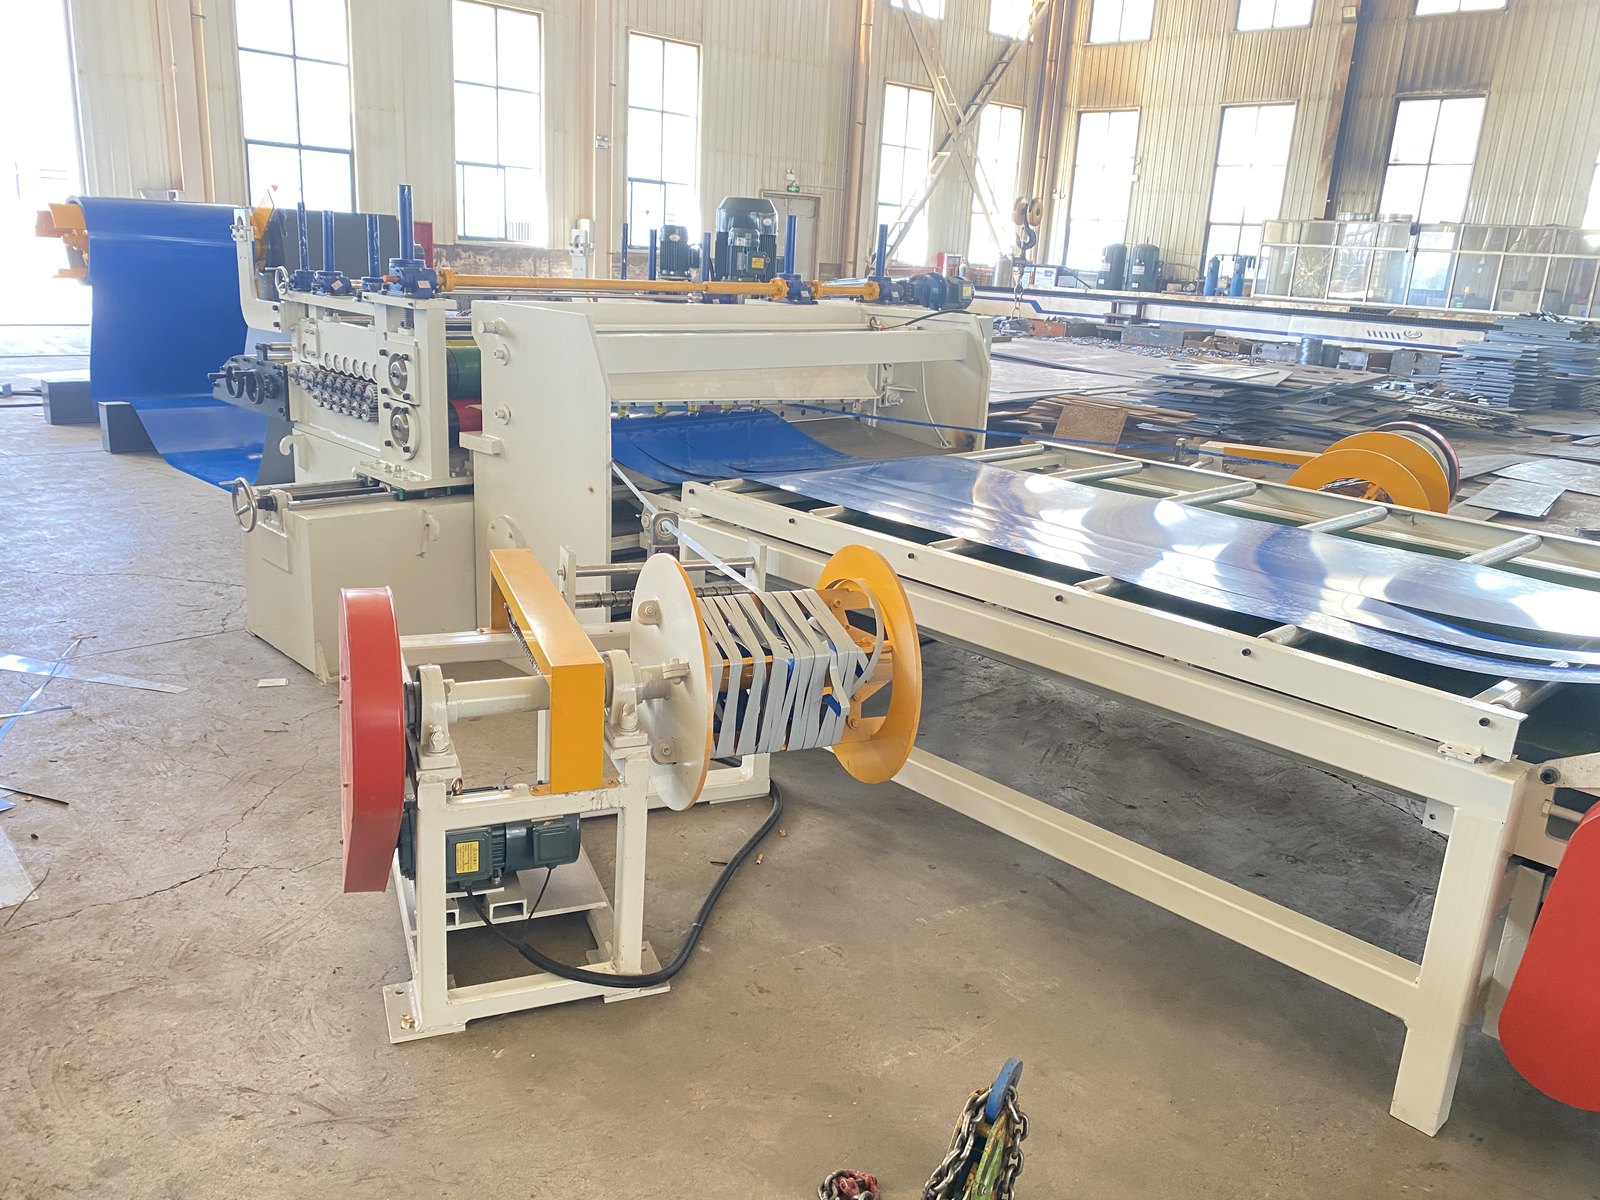
Line composition
- Hydraulic expanding-mandrel decoiler
- Levelling, cut-to-length and slitting combined unit
- Edge trimmer (scrap winder)
- Tension station
- Recoiler
- Unloading car
- Hydraulic and pneumatic power unit
- PLC electrical control system
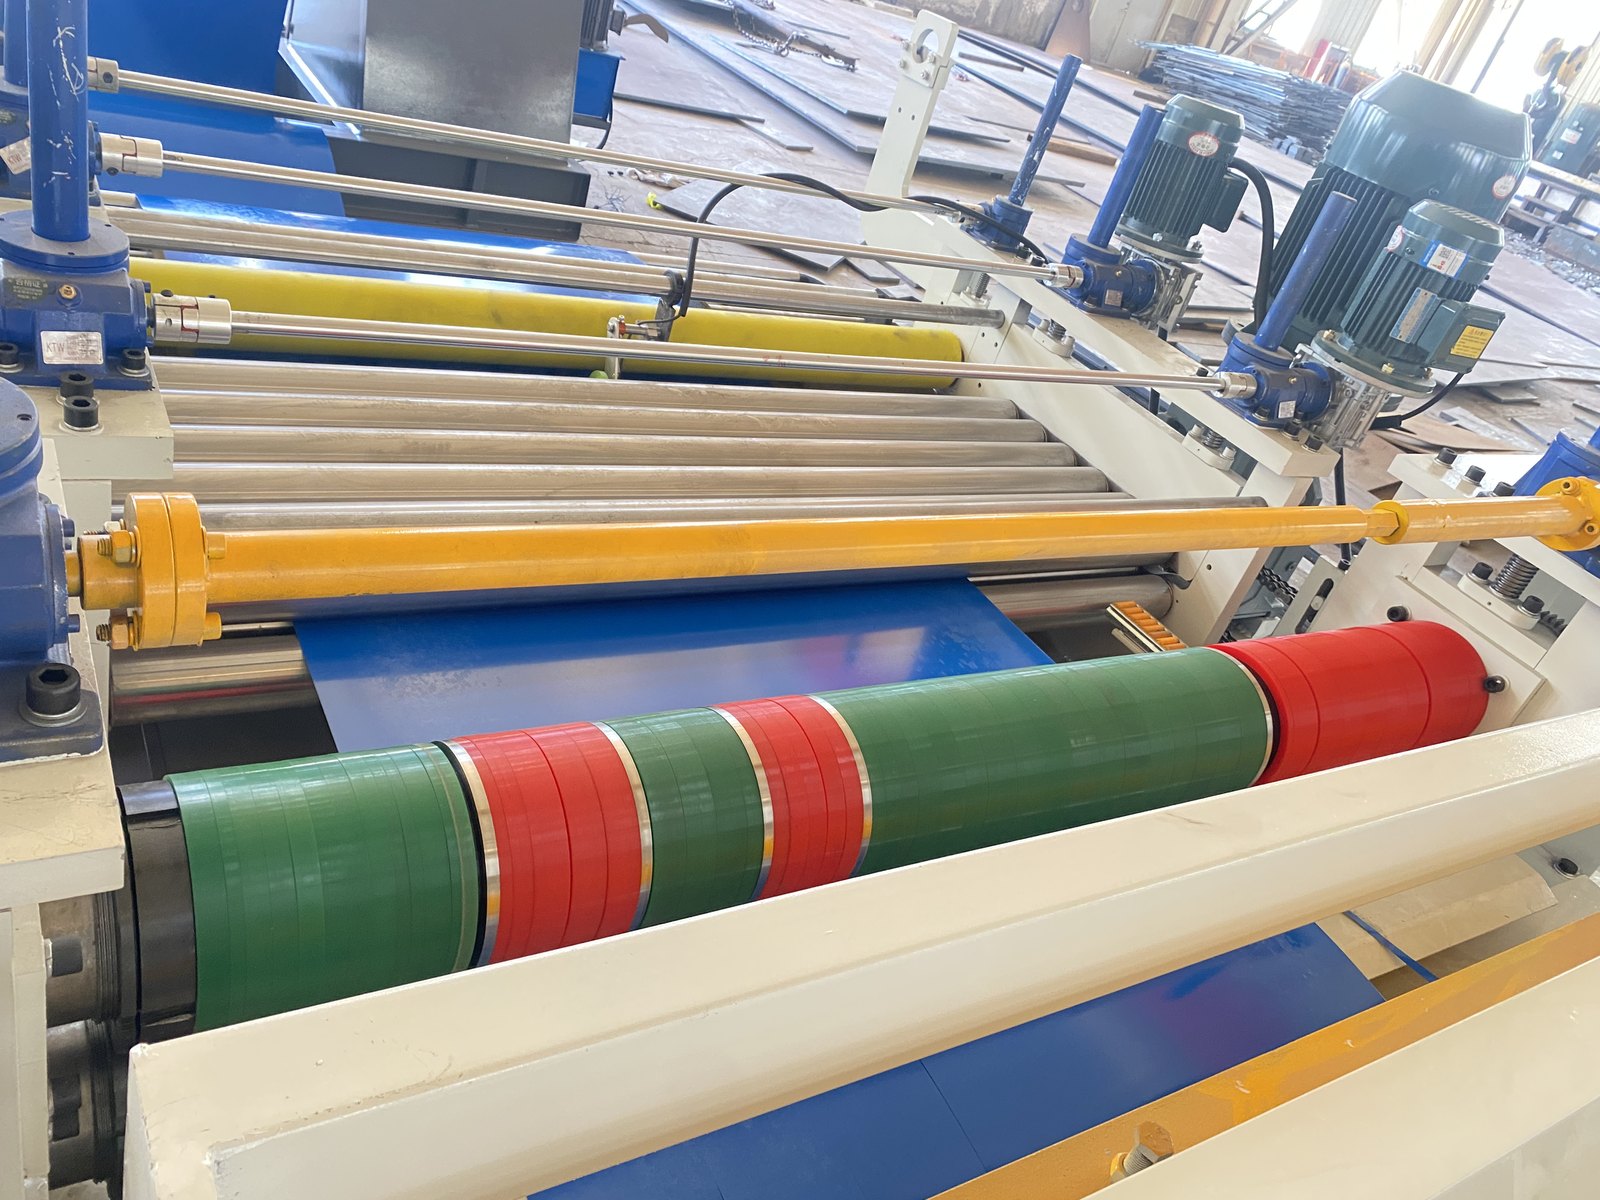
Leveller and slitting head
The leveller uses 17 rolls in a 7-over / 8-under arrangement plus one guide shaft. Roll diameter is 100 mm over a 1250 mm face width, in 40Cr steel, high-frequency hardened and hard chrome plated. Two rows of 90 mm support rolls in 45# steel are adjusted by wedge, so the levelling rolls do not deflect under load.
The slitting head consists of a fixed frame, a movable frame, a lifting unit and the knife shafts. The movable frame travels on a rail base driven by an AC motor, which gives access for changing knife discs, spacers and shims. The lifting unit raises the upper knife shaft through a worm gear and screw; the depth of cut is fine-adjusted by hand. Interchangeable spacer combinations set the finished strip width.
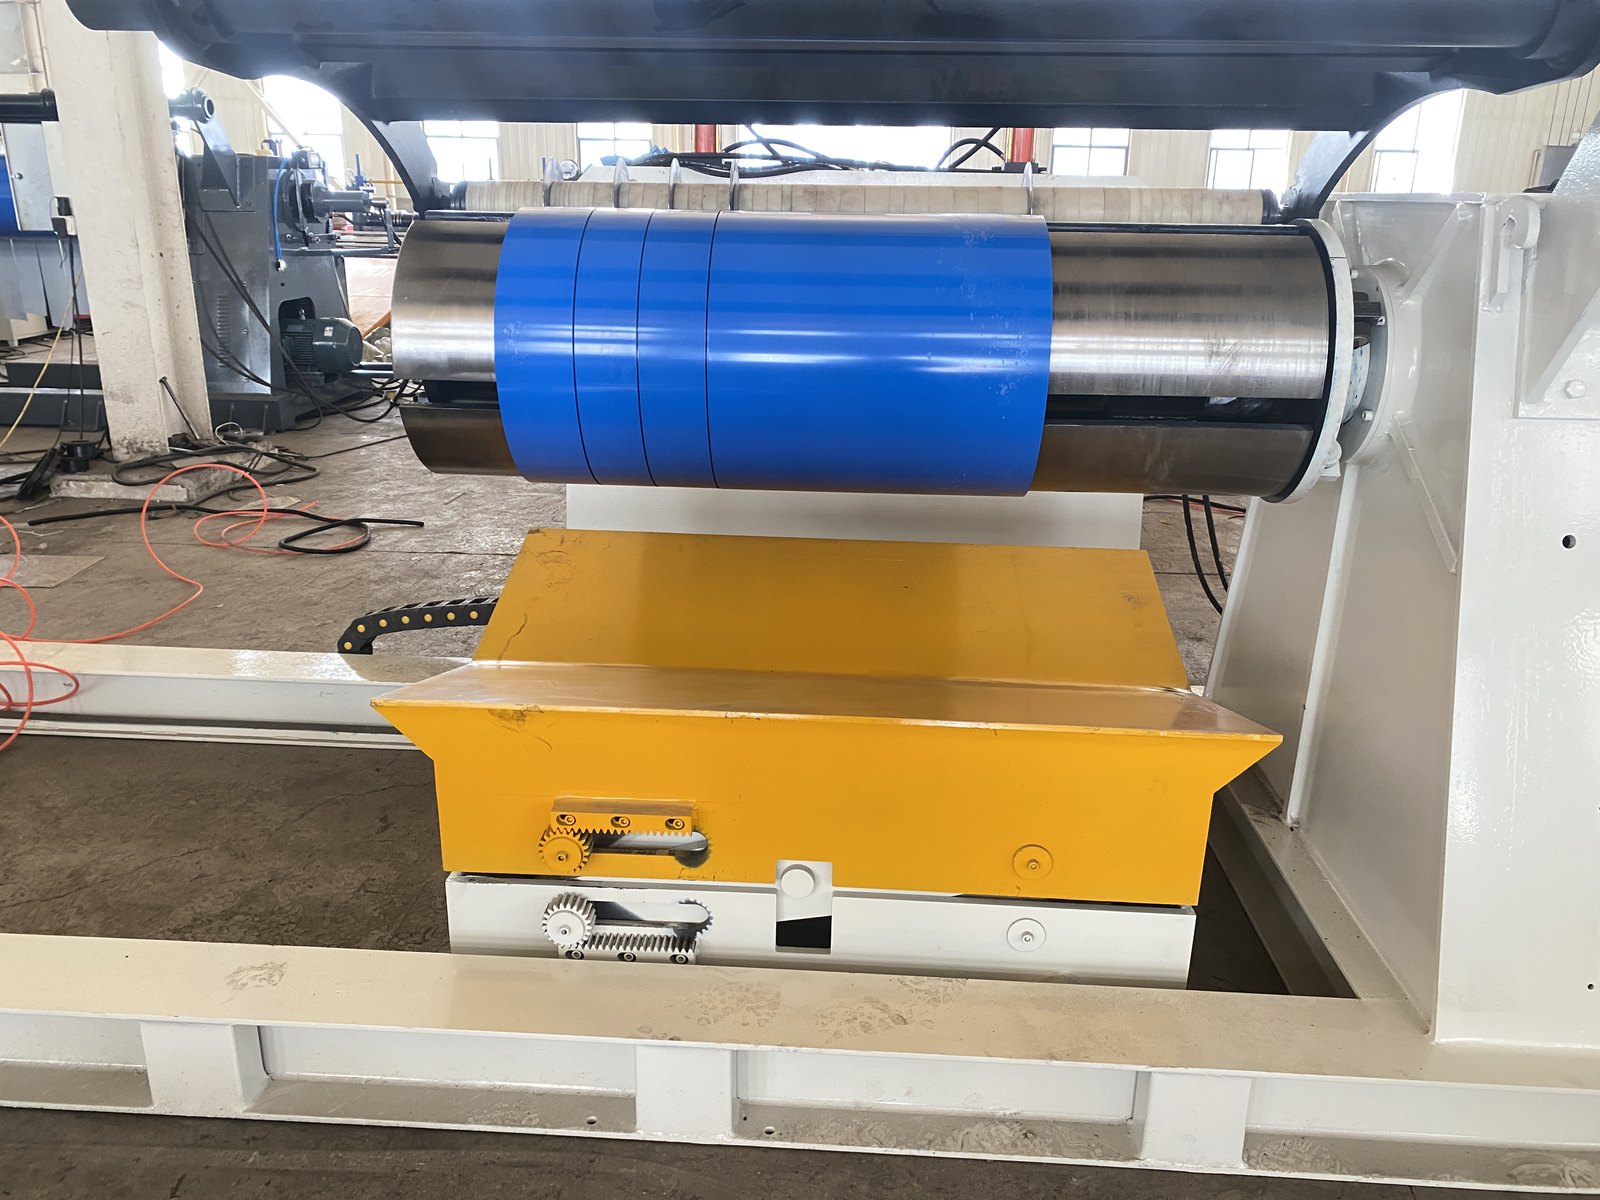
Decoiler
The 1250 mm configuration uses a hydraulic expanding mandrel: 475-525 mm expansion range, 194 mm main shaft, 1250 mm effective mandrel length, 7.5 kW centre drive and a 125 mm expanding cylinder working at 12 MPa. The 1600 mm configuration uses a single-head cantilever decoiler with an anti-loosening hold-down arm and a support arm, working at up to 30 m/min and carrying coils from 2 t to 15 t.
Electrical and control
Decoiler, leveller, shear and recoiler use full-digital AC drives with the whole line under PLC control. The system includes overload protection, circuit-breaker protection and emergency stop. Line interlocks and fault alarms are handled by the PLC, process parameters can be preset, and key machine parameters are monitored with alarms. Shearing speed, coiling tension, length setting, single-machine adjustment and full-line automatic running are all operated from the main console.
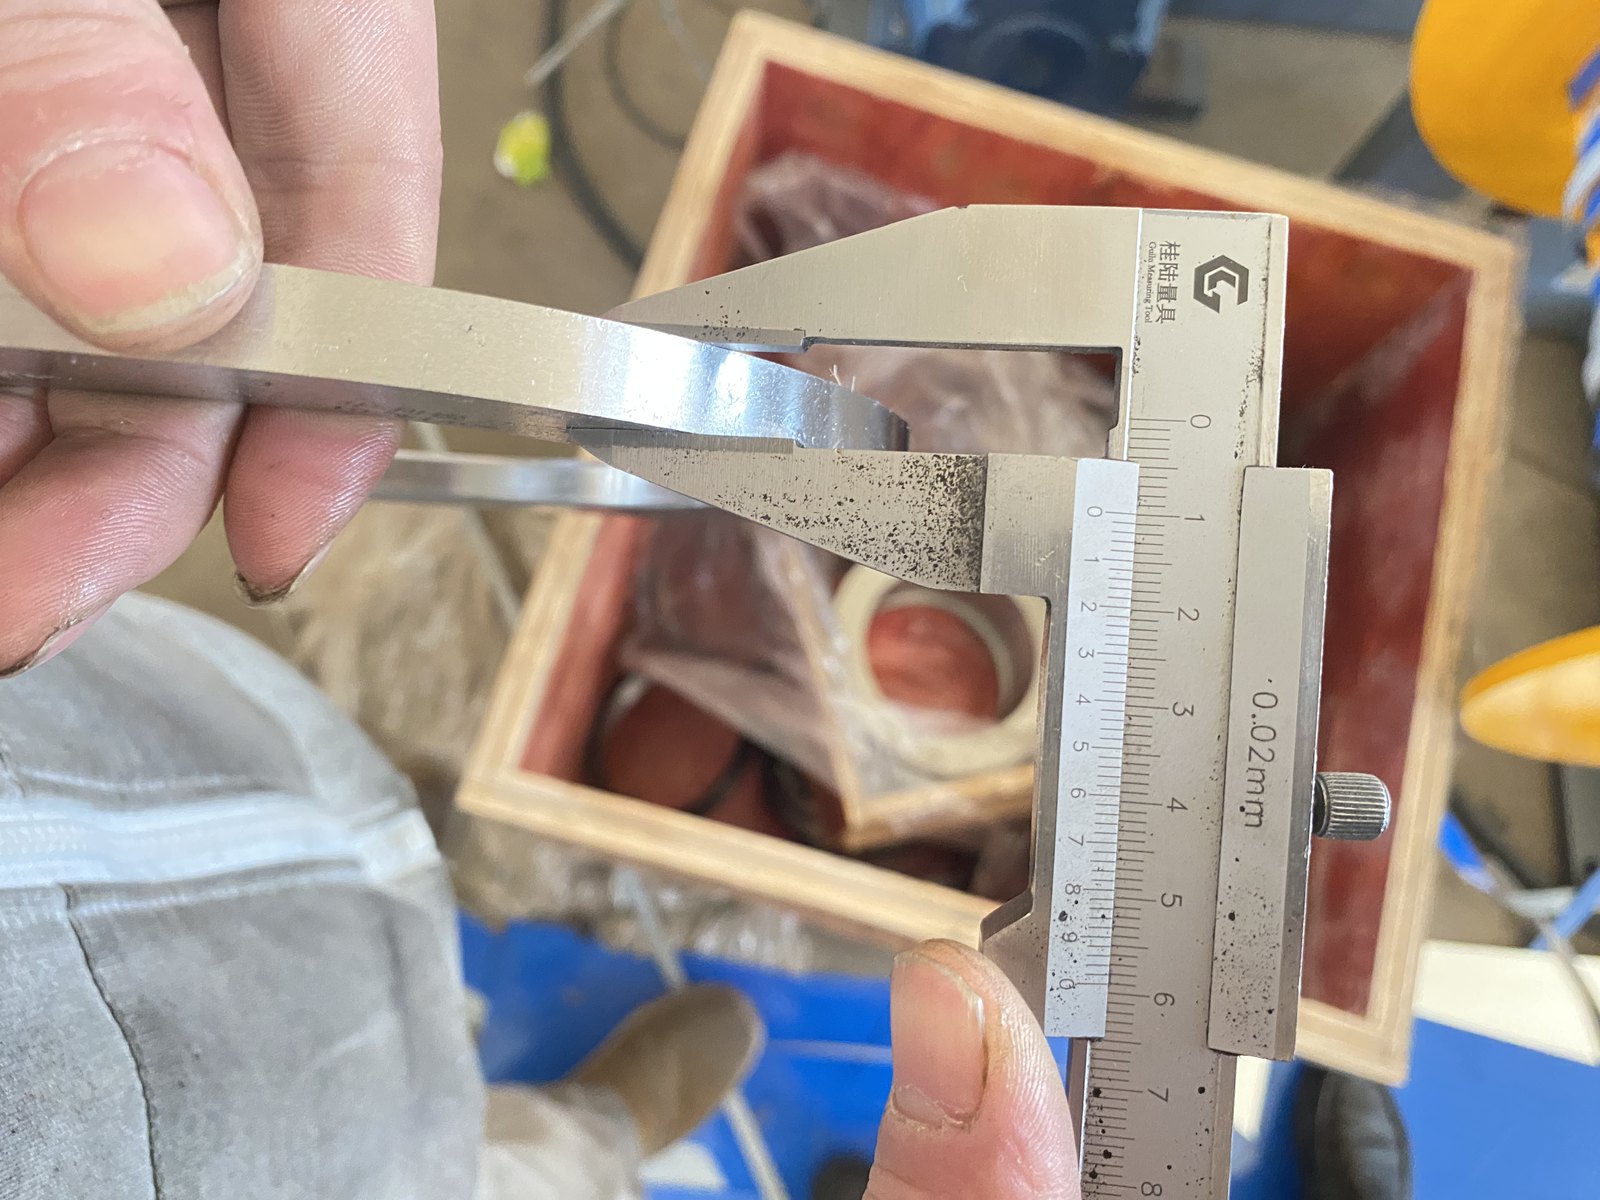
Quality check before dispatch
Width tolerance is verified on the finished strip and the slit edges are checked before the line is packed. Body colour and the operating language of the control system follow your requirement.
What we need from you
To quote the right configuration, tell us the strip material and grade, the thickness range, the incoming coil width, coil inner and outer diameter, coil weight, the strip widths you need to produce, and your supply voltage and frequency.